Welcome to the official website of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in advanced powder handling solutions. Based in Shandong, China, our company, commonly known as HeadPowder, has been dedicated to providing high-quality, efficient, and reliable mobile powder conveying systems for various industrial applications. This article aims to explore the concept of mobile powder conveying systems and delve into the fundamental design principles that underpin their functionality and performance.
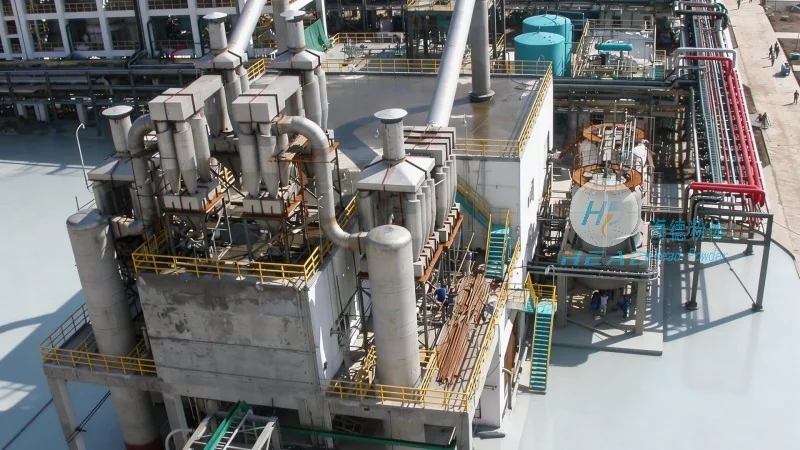
A mobile powder conveying system, as the name suggests, is a flexible and portable equipment designed to transport bulk powders from one location to another. Unlike traditional fixed conveyors, these systems are engineered to be easily moved and reconfigured, making them ideal for applications where the processing site or material source may change frequently. The primary goal of such systems is to ensure the safe, efficient, and hygienic transfer of powders, which are often sensitive materials in industries like pharmaceuticals, food processing, and chemical manufacturing.
The design of a mobile powder conveying system involves several critical principles that ensure its effectiveness and adaptability. First, the system must prioritize material handling efficiency, minimizing downtime and maximizing throughput. This is achieved through the integration of robust components such as high-capacity feeders, durable hoses or flexible pipes, and powerful vacuum or pressure pumps. The choice of conveying method—whether pneumatic (air-assisted) or mechanical (like screw or belt conveyors)—is a key design decision that depends on the properties of the powder, including its density, flowability, and moisture content.
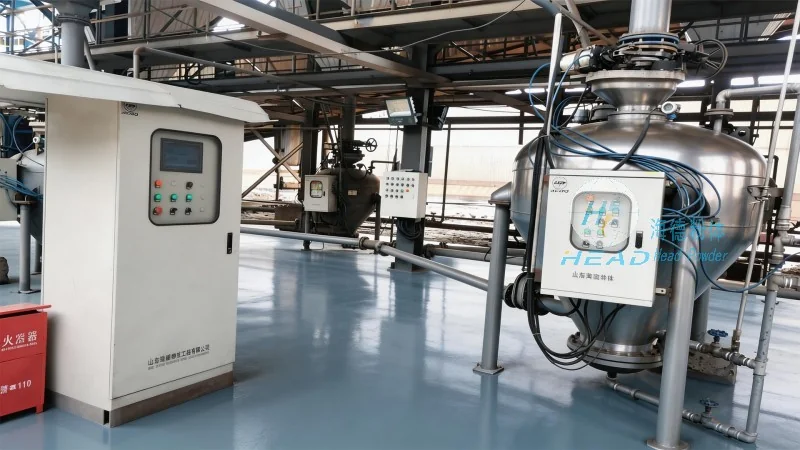
Second, mobility is a core design feature. Mobile systems are typically equipped with wheels or skids that allow for easy relocation. The design must consider the weight distribution and stability of the unit to ensure safe movement and operation on different terrains. Additionally, the system's compactness and modular design enable quick assembly and disassembly, facilitating on-site adjustments as needed. This flexibility is particularly valuable in industries where production lines may need to be reconfigured or where materials are processed in temporary or mobile settings.
At the heart of a mobile powder conveying system are several key components that work in tandem to achieve reliable operation. The feeding mechanism, often a rotary valve or a screw feeder, ensures a consistent and controlled flow of powder into the conveying line. The conveying medium, whether air or mechanical force, is managed by a powerful pump or motor that generates the necessary pressure or vacuum. For pneumatic systems, the air filtration and drying system is crucial to prevent moisture contamination and maintain the quality of the conveyed powder. The system also includes control panels and sensors that monitor pressure, flow rate, and other parameters, providing real-time feedback and allowing for automated adjustments.
Mobile powder conveying systems find extensive applications across various industries due to their adaptability and efficiency. In the pharmaceutical sector, these systems are used to transport raw materials and finished products, ensuring compliance with stringent hygiene and contamination control standards. In the food industry, they facilitate the handling of dry ingredients like flour, sugar, and spices, maintaining product quality and safety. The chemical industry also benefits from these systems for transporting powders such as catalysts, pigments, and reagents, where precise control over material flow is essential. Additionally, in construction and mining, mobile conveying systems are used for transporting bulk materials like cement, sand, and gravel, enhancing operational flexibility on job sites.
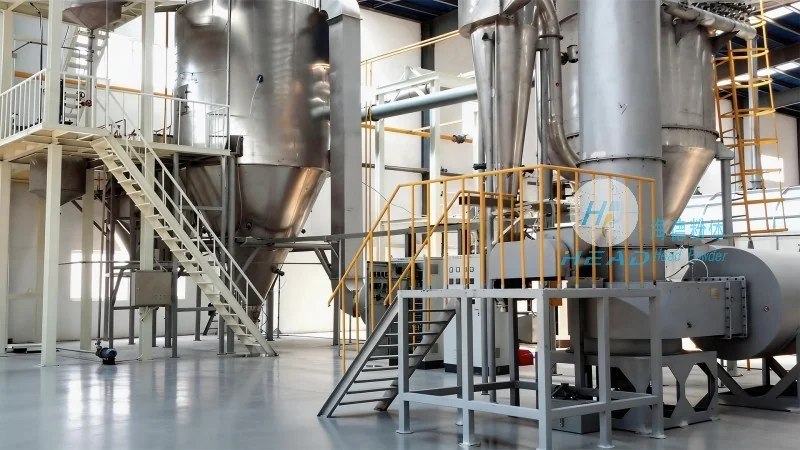
Compared to traditional fixed conveyors, mobile powder conveying systems offer several advantages that make them a preferred choice in many applications. First, their portability allows for greater flexibility in production planning and site management. Companies can easily reconfigure their processing lines without the need for extensive infrastructure changes, reducing capital expenditure and time. Second, the modular design of these systems enables easy maintenance and repair, as components can be replaced or serviced without disrupting the entire operation. This leads to lower downtime and higher overall system reliability. Third, the ability to handle a wide range of powder types and sizes makes mobile systems versatile, catering to diverse industrial needs. Finally, the integration of advanced control technologies enhances operational efficiency and safety, ensuring that the conveying process is optimized for performance and compliance with industry standards.
In conclusion, a mobile powder conveying system is a sophisticated piece of equipment designed to meet the evolving needs of modern industrial processes. The design principles, including efficiency, mobility, and adaptability, are carefully integrated to provide reliable and effective powder handling solutions. As a leading manufacturer based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and refine these systems to meet the demands of various industries, ensuring that businesses can achieve optimal performance and operational flexibility in their powder handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top