Intelligent bulk material pneumatic conveying systems represent a sophisticated solution for the efficient handling and transportation of dry powders and granules in industrial settings. These systems are engineered to provide reliable, flexible, and automated material transfer processes, which are critical for maintaining productivity and operational efficiency in various industries such as food processing, pharmaceuticals, chemicals, and mining.
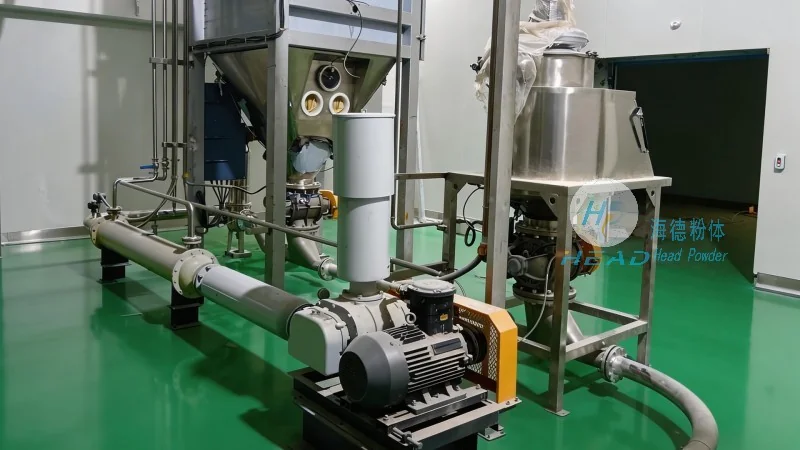
At the core of these systems is the ability to transport bulk materials through a pipeline using air or other gases as the conveying medium. The technology integrates advanced control systems, sensors, and automation to ensure precise material flow, consistent pressure, and optimal energy consumption. This intelligent approach not only enhances operational safety but also reduces downtime and maintenance costs, making it a preferred choice for modern industrial applications.
The intelligent pneumatic conveying system typically consists of several key components, each playing a crucial role in the overall operation. These include the material feed hopper, which stores and feeds the bulk material into the system; the air compressor or blower, which generates the necessary pressure to move the material; the conveying line, which transports the material from the source to the destination; and the control unit, which monitors and adjusts the system parameters in real-time. Additionally, features like dust collection systems and material separation units are often integrated to ensure environmental compliance and product purity.
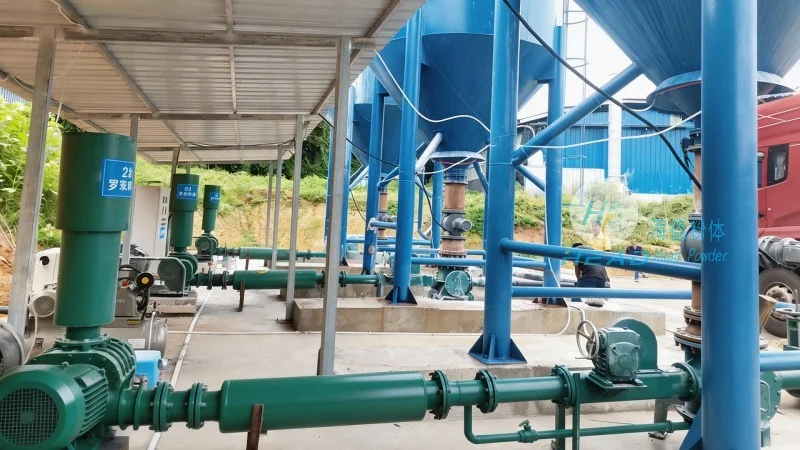
The design of an intelligent pneumatic conveying system involves careful consideration of several factors to ensure optimal performance and reliability. The system's design must account for the physical properties of the material being conveyed, such as particle size, density, and moisture content, as these characteristics directly impact the conveying velocity and pressure requirements. Engineers also consider the system's layout, including the length and diameter of the conveying line, the number of bends and fittings, and the placement of components to minimize pressure losses and energy consumption. Furthermore, the integration of intelligent control systems allows for adaptive adjustments based on real-time data, ensuring the system operates at peak efficiency under varying conditions.
Implementing an intelligent pneumatic conveying system offers numerous benefits to industrial operations. One of the primary advantages is the reduction in labor costs and manual handling, as the system automates the entire material transfer process. This not only improves safety by minimizing human exposure to hazardous materials but also enhances product quality by reducing contamination and segregation. Additionally, the system's flexibility allows for easy integration with existing production lines and the ability to handle a wide range of materials without significant modifications. The energy efficiency of these systems, combined with lower maintenance requirements, results in long-term cost savings and increased profitability for businesses.
Intelligent pneumatic conveying systems are widely used across various industries due to their adaptability and efficiency. In the food and beverage industry, these systems are employed to transport ingredients like flour, sugar, and spices with strict hygiene standards. The pharmaceutical industry utilizes them for the handling of active pharmaceutical ingredients (APIs) and other sensitive materials, where contamination control is paramount. In the chemical industry, they are used to convey powders and granules in processes involving reactive or hazardous substances, ensuring safe and controlled material transfer. The mining and minerals sector also benefits from these systems for transporting raw materials and byproducts, improving the overall efficiency of extraction and processing operations.
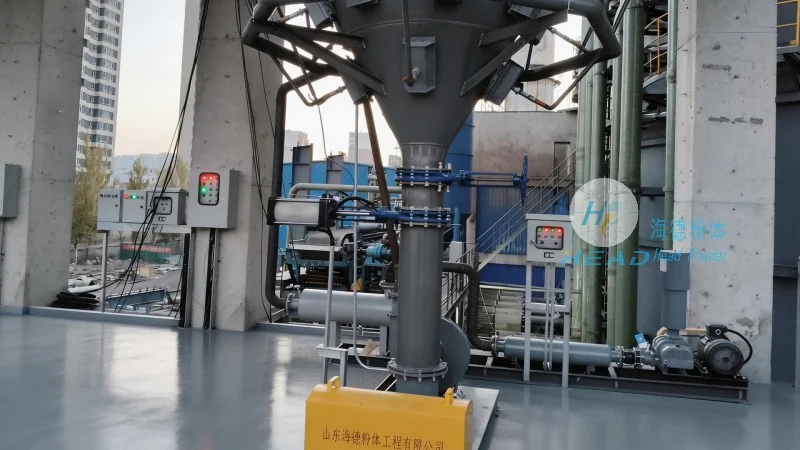
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing customized intelligent pneumatic conveying systems tailored to the specific needs of each client. The company's expertise lies in understanding the unique challenges of different industries and providing solutions that address these challenges effectively. Whether it's a small-scale system for a laboratory or a large-scale system for an industrial plant, HeadPowder offers scalable solutions that can be expanded or modified as operational needs evolve. The company's commitment to quality and innovation ensures that each system is built to meet the highest standards of performance and reliability.
Intelligent pneumatic conveying systems represent a significant advancement in material handling technology, offering efficient, safe, and cost-effective solutions for the transportation of bulk materials. With their advanced design principles and intelligent control systems, these systems are essential for modern industrial operations. As industries continue to demand higher efficiency and productivity, the role of intelligent pneumatic conveying systems will only grow, making them a critical component in the future of industrial material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top