Deeply engaged in industrial bulk material scenarios, providing integrated intelligent environmental solutions for automatic batching, centralized feeding, dry desulfurization and denitrification!
Your current position:首页 >> News >> Company News

What is Urea Pneumatic Conveying? And What Are Its Design Principles?

Release time:2026-09-14 10:52:26
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang

Urea, a vital nitrogen fertilizer, is commonly transported using pneumatic conveying systems. This method involves moving urea particles through a pipeline using air or other gases as the conveying medium. The process is efficient and can handle large volumes of material, making it a preferred choice in the fertilizer industry. Understanding the fundamentals of urea pneumatic conveying and its design principles is essential for optimizing operations and ensuring reliable material transport.
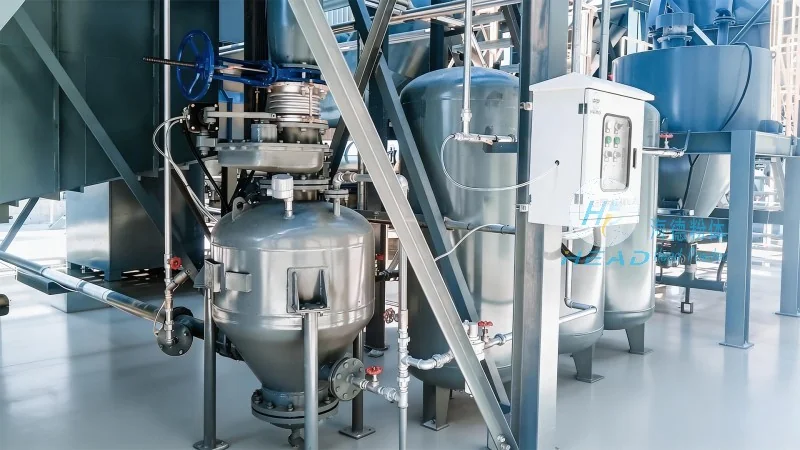
What is Urea Pneumatic Conveying? And What Are Its Design Principles?

What is Urea Pneumatic Conveying?

Urea pneumatic conveying is a technology that utilizes air or gas to transport urea granules or powder through a closed pipeline system. Unlike traditional mechanical conveying methods like screw conveyors or belt conveyors, pneumatic systems rely on the kinetic energy of the conveying medium to move the material. This approach is particularly advantageous for handling fine or dusty materials like urea, as it minimizes product degradation and reduces the risk of contamination.

The Core Components of a Urea Pneumatic Conveying System

A typical urea pneumatic conveying system consists of several key components that work in tandem to ensure efficient material transport. The primary components include:
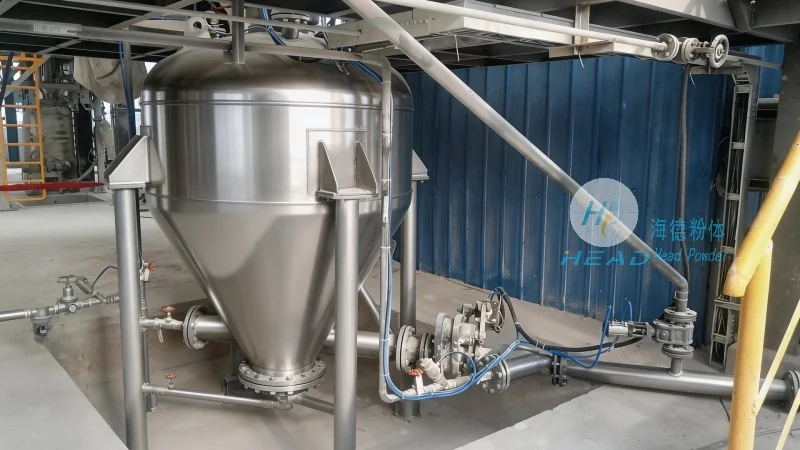
What is Urea Pneumatic Conveying? And What Are Its Design Principles?

  • Conveying Pipeline: A network of pipes designed to carry the urea particles and conveying medium. The pipeline is usually made of materials like stainless steel or plastic, chosen for their resistance to corrosion and wear from urea particles.
  • Air or Gas Source: A blower or compressor that generates the necessary airflow or gas pressure to move the urea. The choice of air source depends on the system's capacity and the required pressure levels.
  • Feed Hopper: A container that holds the urea before it is introduced into the pipeline. The hopper is equipped with a feeder mechanism, such as a rotary valve or a screw feeder, to control the flow rate of the urea into the system.
  • Separation and Collection Equipment: At the receiving end of the pipeline, a separator (like a cyclone or bag filter) is used to separate the urea particles from the conveying medium. The separated urea is then collected in a storage bin or silo.
  • Control System: A set of sensors and controls that monitor and regulate the system's operation. This includes pressure sensors, flow meters, and control valves to maintain optimal conditions and prevent system failures.

Design Principles for Urea Pneumatic Conveying Systems

The design of a urea pneumatic conveying system is based on several critical principles to ensure efficient and reliable operation. These principles are tailored to the physical properties of urea, such as its particle size, density, and flow characteristics.

First, the system must maintain a consistent air velocity within the pipeline. The velocity is typically kept above the "minimum conveying velocity" to prevent the urea particles from settling or clogging the pipeline. For urea, this velocity often ranges from 15 to 25 meters per second, depending on the particle size and system configuration.

Second, the pressure drop across the system must be minimized to reduce energy consumption. The design considers factors like pipeline length, diameter, and the number of bends or fittings, as these elements contribute to pressure losses. Engineers use computational fluid dynamics (CFD) and empirical formulas to calculate the optimal pipeline dimensions and layout.
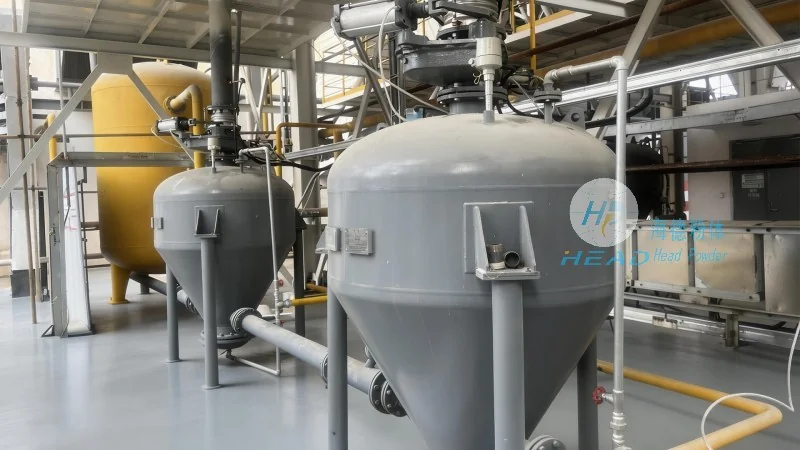
What is Urea Pneumatic Conveying? And What Are Its Design Principles?

Third, the system must account for the abrasive nature of urea particles. The materials used for the pipeline and components (e.g., stainless steel, special alloys) are selected to withstand wear and corrosion from the urea. Regular maintenance and inspection are also critical to prevent system degradation.

Fourth, the design incorporates safety features to handle potential issues like blockages or overpressure. For example, the system may include pressure relief valves and emergency shut-off mechanisms to prevent accidents and ensure operator safety.

Key Design Considerations for Urea Pneumatic Conveying

When designing a urea pneumatic conveying system, several factors must be carefully considered to ensure optimal performance and longevity. These considerations include:
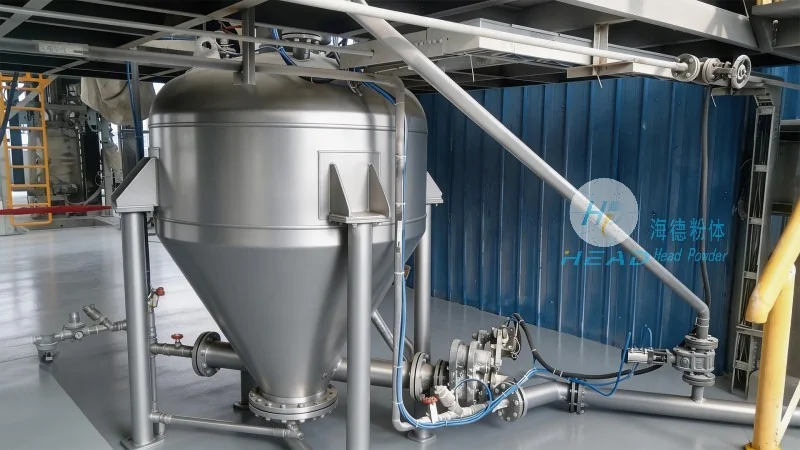
What is Urea Pneumatic Conveying? And What Are Its Design Principles?

  • Particle Size and Distribution: The size and uniformity of urea particles affect the system's design. Finer particles require higher air velocities and more efficient separation equipment to prevent clogging.
  • System Capacity and Throughput: The required volume of urea to be transported dictates the size of the pipeline, blower capacity, and feeder speed. A larger system may need multiple pipelines or a larger blower to handle higher throughput.
  • Pipeline Layout and Obstacles: The physical layout of the facility, including the distance between the feed and receiving points, and any obstacles (e.g., buildings, equipment), influences the system's design. The pipeline may need to be elevated or use vertical sections to overcome elevation changes.
  • Energy Efficiency: The design aims to minimize energy consumption by optimizing air velocity, reducing pressure losses, and using efficient components. This not only lowers operational costs but also aligns with sustainability goals.
  • Material Compatibility: The materials used for the pipeline, components, and separation equipment must be compatible with urea to prevent chemical reactions or corrosion. Stainless steel and certain plastics are commonly used for their resistance to urea.

Applications and Benefits of Urea Pneumatic Conveying

Urea pneumatic conveying systems are widely used in the fertilizer industry for transporting urea from production facilities to storage or distribution centers. The benefits of this technology include:

  • Efficient Material Handling: Pneumatic systems can transport large volumes of urea quickly and efficiently, reducing labor costs and increasing productivity.
  • Reduced Product Degradation: Unlike mechanical conveyors, pneumatic systems minimize product degradation by avoiding direct contact with moving parts or high friction.
  • Improved Safety: The enclosed pipeline system reduces dust emissions and the risk of accidents, making it safer for operators and the environment.
  • Flexibility in Layout: Pneumatic systems can be easily reconfigured or expanded to accommodate changes in production or storage needs.
  • Lower Maintenance Costs: With fewer moving parts compared to mechanical conveyors, pneumatic systems require less maintenance and have longer service lives.

Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing customized urea pneumatic conveying systems. With years of experience in the industry, the company ensures that its systems are tailored to meet the specific needs of clients, whether for small-scale or large-scale fertilizer operations. The company's headquarters is located in Shandong, China, and it serves clients globally with reliable and efficient urea conveying solutions.

recommend

Copyright © Shandong Headpowder Engineering Co., Ltd. All Rights Reserved.    营业执照公示 网站地图

top
