Quartz stone, a widely used material in various industries, often requires efficient and reliable transportation methods to ensure smooth production processes. The principle of pneumatic conveying equipment for quartz stone is a critical aspect of material handling technology, enabling the safe and effective movement of this abrasive and valuable material from one location to another.
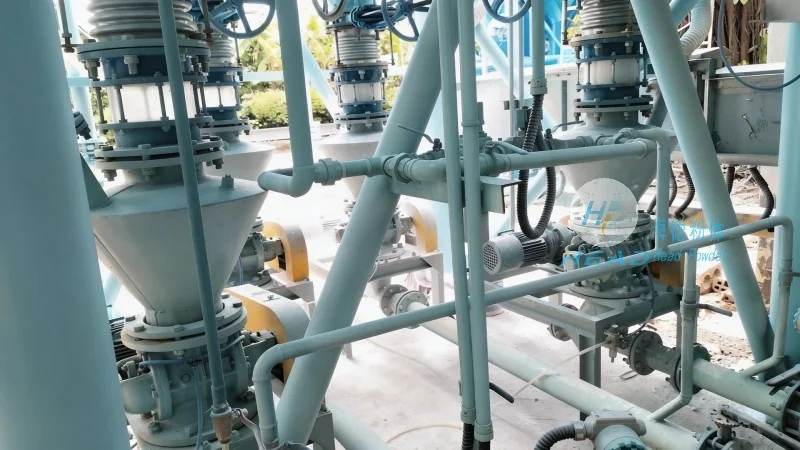
The fundamental concept behind quartz stone pneumatic conveying involves using air as the medium to transport solid particles. This method, known as pneumatic conveying, utilizes a pressure differential or vacuum to move the quartz particles through a pipeline system. The process typically involves a hopper where quartz stone is fed into the system, followed by an air compressor that generates the necessary pressure to propel the material forward. As the air flows through the pipeline, it carries the quartz particles along, ensuring they are transported without the need for mechanical components like belts or buckets that might be prone to wear and tear from the abrasive nature of quartz.
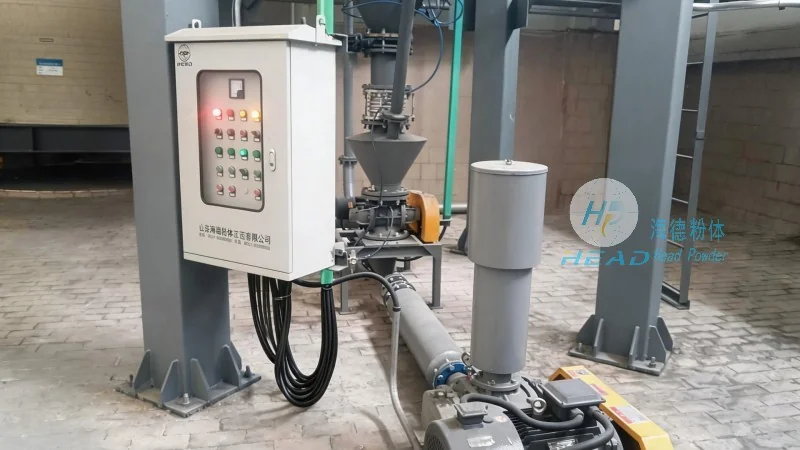
Several key components work together to ensure the efficient operation of quartz stone pneumatic conveying equipment. The first component is the hopper, which serves as the storage and feeding unit for the quartz stone. It is designed to maintain a consistent flow of material into the conveying system, preventing blockages and ensuring a steady supply. The second critical component is the air compressor, which generates the pressure required to move the material. Different types of compressors, such as positive displacement or centrifugal models, are used depending on the system's capacity and the characteristics of the quartz stone. The third component is the pipeline system, which consists of pipes that transport the quartz particles along with the air. These pipes are typically made of materials resistant to abrasion, such as stainless steel or special plastic composites, to withstand the wear caused by the quartz particles. Additionally, the system includes a separator or cyclone, which separates the quartz particles from the air at the end of the pipeline. This separator is crucial for recovering the material and ensuring that the air can be recycled or vented safely.
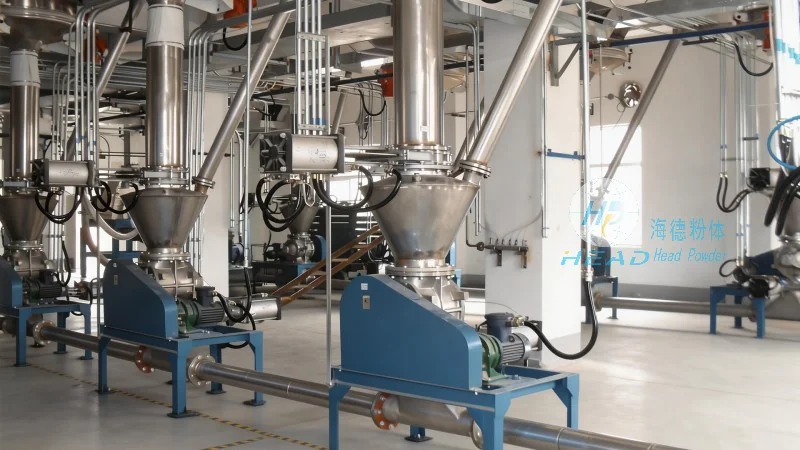
Implementing pneumatic conveying for quartz stone handling offers several advantages over traditional methods. Firstly, it provides a dust-free environment, which is essential for maintaining workplace safety and compliance with environmental regulations. Unlike mechanical conveying systems that can generate significant dust, pneumatic conveying keeps the material enclosed within the pipeline, reducing airborne particles and improving air quality. Secondly, it offers high efficiency in material transport, with the ability to move large quantities of quartz stone over long distances with minimal energy consumption. The system's design allows for continuous operation, reducing downtime and increasing overall productivity. Thirdly, it is highly flexible, as the pipeline can be easily reconfigured or extended to accommodate changes in production needs or facility layout. This flexibility makes it suitable for various applications, from small-scale operations to large industrial plants. Lastly, the system is relatively low maintenance compared to mechanical systems, as there are fewer moving parts that can wear out or require frequent replacement.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of pneumatic conveying equipment for various industrial applications, including quartz stone handling. With a strong commitment to quality and innovation, the company specializes in designing and manufacturing custom solutions tailored to the specific needs of its clients. Headpowder's team of experienced engineers and technicians leverages advanced technology and rigorous testing to ensure that each product meets the highest standards of performance and reliability. The company's facilities, located in Shandong, China, are equipped with state-of-the-art manufacturing equipment and quality control systems, enabling the production of durable and efficient pneumatic conveying systems. Headpowder's products are known for their durability, energy efficiency, and ease of maintenance, making them a preferred choice for industries that require reliable material handling solutions.
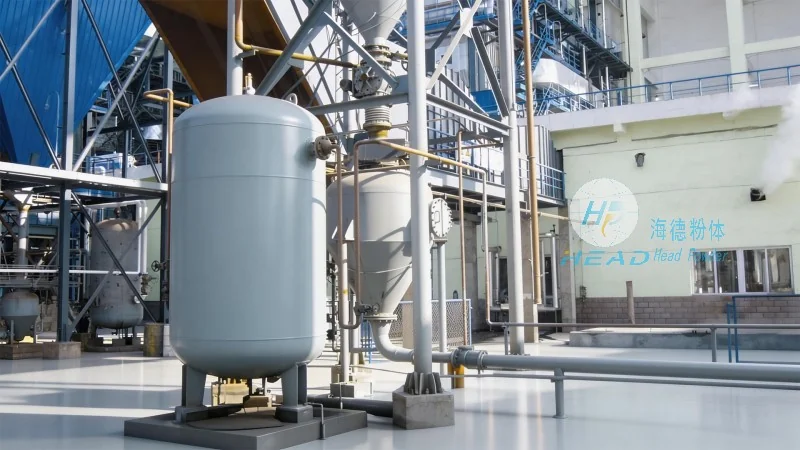
In conclusion, the principle of quartz stone pneumatic conveying is a vital technology for industries dealing with this valuable and abrasive material. By understanding the core components and advantages of such systems, businesses can enhance their operational efficiency, improve workplace safety, and reduce maintenance costs. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in providing high-quality pneumatic conveying equipment that meets the specific requirements of quartz stone handling, ensuring that industries can achieve optimal performance and productivity. As the demand for efficient material handling solutions continues to grow, the importance of pneumatic conveying in quartz stone processing will only increase, making it an essential technology for modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top