HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design and implementation of advanced pneumatic conveying systems for powder materials. This article delves into the fundamental principles underlying the operation of a powder electrolyte pneumatic conveying system, highlighting the technical aspects and operational efficiency that define such systems.
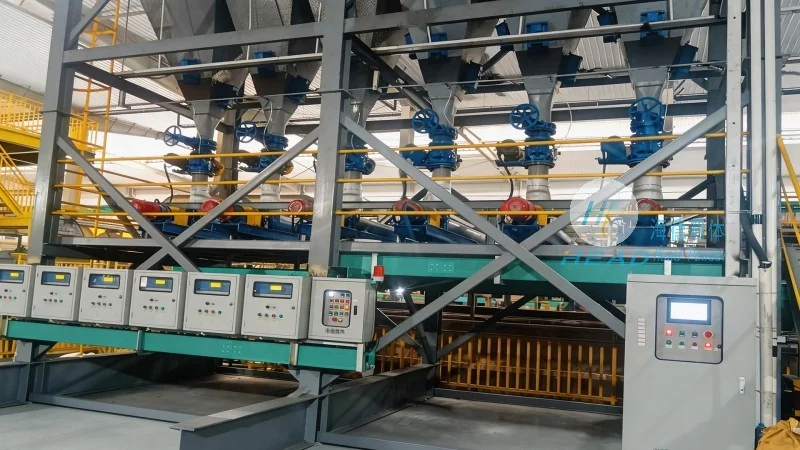
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has established itself as a trusted provider of customized material handling equipment, focusing on innovative solutions that meet the diverse needs of industrial clients. With a commitment to quality and technological advancement, HeadPowder delivers reliable systems that enhance productivity and safety in material transport processes.
Pneumatic conveying systems utilize air or other gases to transport bulk materials, such as powders, granules, and fine particles, from one location to another. In the context of powder electrolytes—materials commonly used in battery manufacturing, chemical processing, and other industrial applications—the efficiency of material transport is critical for maintaining production line continuity and product quality. The core principle of pneumatic conveying involves creating a pressure differential between the conveying line and the ambient environment, which propels the material through the system using air flow.
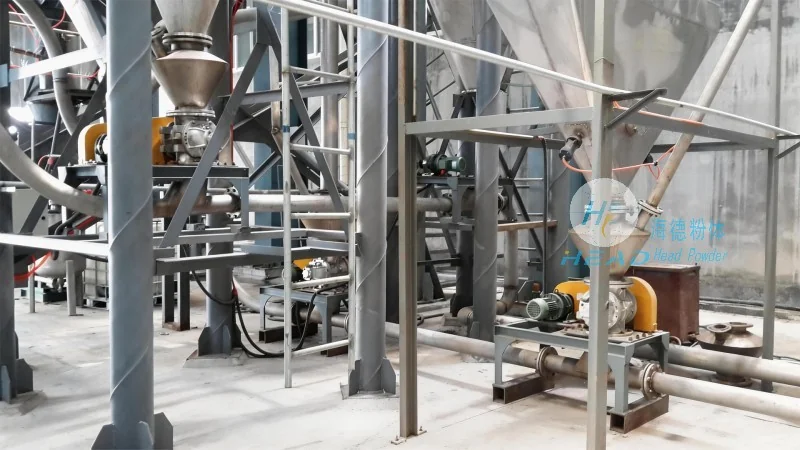
A typical powder electrolyte pneumatic conveying system comprises several essential components, each playing a vital role in the overall operation. These include the material feed hopper, which stores and regulates the flow of the powder electrolyte; the air compressor or blower, which generates the necessary air pressure; the conveying line, which transports the material; and the discharge device, which delivers the material to its final destination. The system operates by introducing the powder electrolyte into the conveying line at a controlled rate, while simultaneously supplying compressed air. The air flow creates a negative pressure or positive pressure environment, depending on the system design, to move the material through the pipeline.
Compared to traditional mechanical conveying methods, pneumatic conveying offers several advantages when handling powder electrolytes. These include the ability to transport materials over long distances without the need for intermediate transfer points, reduced risk of material contamination due to enclosed systems, and improved safety by eliminating the need for manual handling of bulk powders. Additionally, pneumatic systems can handle a wide range of particle sizes and moisture contents, making them versatile for various industrial applications. The efficiency of material transport, combined with lower maintenance requirements compared to mechanical systems, contributes to overall cost savings and operational reliability.
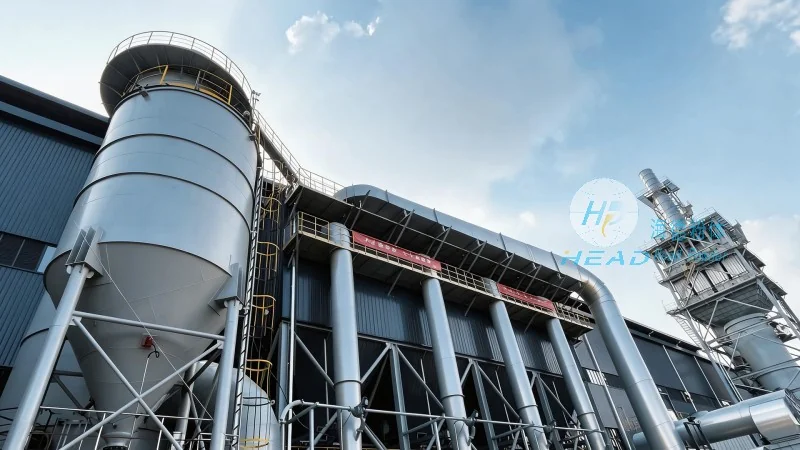
Powder electrolyte pneumatic conveying systems are widely employed in industries where the handling of fine powders is essential. In the battery manufacturing sector, for instance, these systems are crucial for transporting active materials to production lines, ensuring consistent quality and minimizing material loss. In chemical processing, they facilitate the movement of reagents and intermediates between processing stages, enhancing process efficiency. The systems also find applications in pharmaceutical and food processing industries, where maintaining product purity and hygiene is paramount. By providing a clean and controlled environment for material transport, pneumatic systems help meet stringent industry standards and regulatory requirements.
The successful implementation of a powder electrolyte pneumatic conveying system requires careful consideration of several technical factors. These include the selection of appropriate air flow rates and pressure levels to ensure efficient material transport without excessive energy consumption. The design of the conveying line, including pipe diameter, material, and bends, must be optimized to minimize pressure drop and prevent material buildup or blockages. Additionally, the choice of components, such as air filters and moisture separators, is critical to maintain system performance and prevent damage from contaminants. HeadPowder’s expertise in system design and engineering ensures that these factors are addressed comprehensively, resulting in customized solutions tailored to specific client needs.
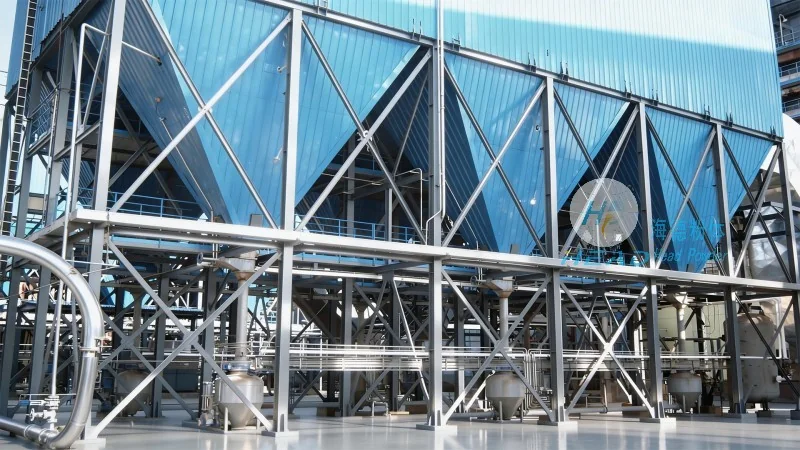
To ensure the long-term reliability and efficiency of a powder electrolyte pneumatic conveying system, regular maintenance and adherence to operational best practices are essential. This includes routine checks of air compressor performance, cleaning of air filters and conveying lines to prevent clogging, and monitoring of material flow rates to detect any deviations from normal operation. Proper training of operators on system operation and troubleshooting is also crucial for maintaining optimal performance. By implementing these practices, industrial facilities can maximize the lifespan of their conveying systems and minimize downtime, thereby enhancing overall productivity and cost-effectiveness.
The principle of powder electrolyte pneumatic conveying systems, as exemplified by solutions from Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated approach to material handling in modern industrial applications. By leveraging the power of air flow to transport fine powders efficiently and safely, these systems address the challenges associated with traditional mechanical conveying methods. With a focus on innovation, quality, and customer-centric solutions, HeadPowder continues to advance the technology of pneumatic conveying, providing reliable and effective systems that meet the evolving needs of industrial clients worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top