Caustic soda, also known as sodium hydroxide (NaOH), is a widely used chemical in various industrial processes. The efficient and safe transportation of caustic soda from storage to processing units is crucial for maintaining operational efficiency and ensuring workplace safety. Pneumatic conveying systems have emerged as a preferred solution for handling caustic soda due to their ability to transport the material in a closed environment, minimizing dust exposure and contamination risks. This article explores the fundamental principles behind caustic soda pneumatic conveying systems, highlighting key components, operational mechanisms, and the benefits they offer to industrial applications.
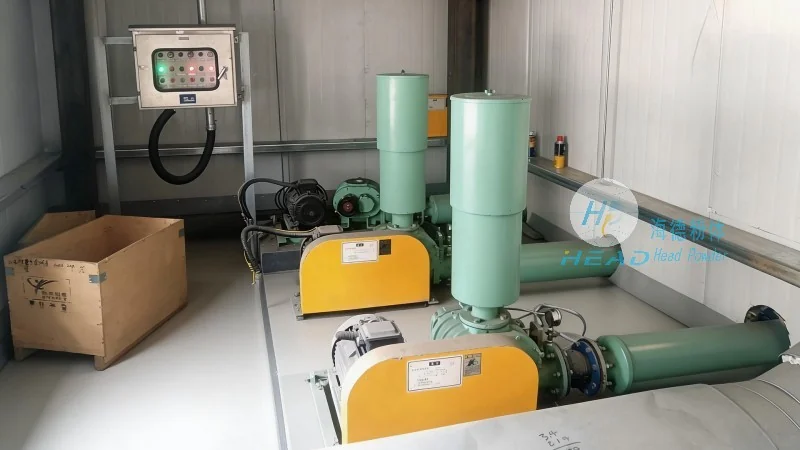
A typical caustic soda pneumatic conveying system consists of several critical components that work in tandem to ensure smooth material transport. The main components include a hopper or storage silo for holding the caustic soda, a feeder mechanism to control the flow rate, a conveying line (usually made of stainless steel or other corrosion-resistant materials to withstand the chemical's properties), a blower or air compressor to generate the necessary air pressure, and a receiver or discharge hopper at the destination. Each component plays a vital role in the overall system performance and reliability.
The core principle of pneumatic conveying is the use of air or gas to move solid materials through a pipeline. In the case of caustic soda, the system operates by creating a flow of air that entrains the solid particles, carrying them from the source to the destination. There are two primary types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems use higher air velocities to transport materials in a suspended state, suitable for shorter distances and lower material loads. Dense-phase systems, on the other hand, use lower air velocities and higher material concentrations, ideal for longer distances and bulk material transport. The choice between these systems depends on factors such as the distance between the source and destination, the material's characteristics, and the required flow rate.
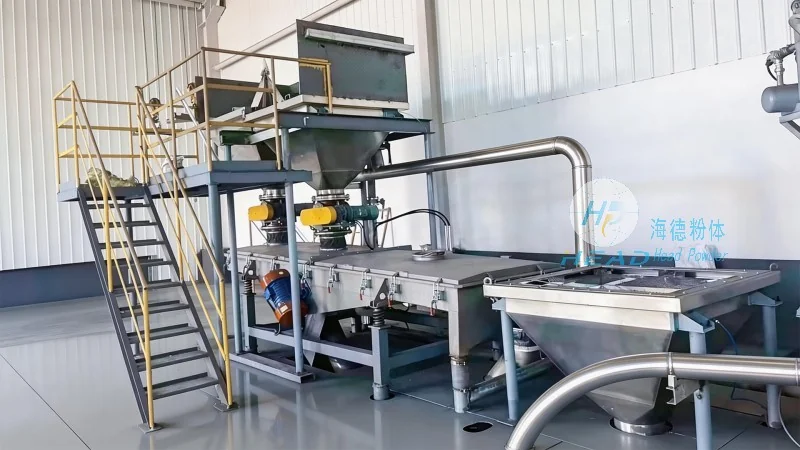
Implementing a pneumatic conveying system for caustic soda offers numerous advantages over traditional methods like bucket elevators or belt conveyors. Firstly, it provides a completely enclosed system, which significantly reduces the risk of dust exposure and environmental contamination. This is particularly important for caustic soda, as it can be hazardous if inhaled or comes into contact with skin. Secondly, pneumatic conveying systems are highly efficient in terms of energy consumption and operational speed, allowing for rapid material transfer with minimal downtime. Thirdly, the system's design allows for easy integration with other processing equipment, enabling seamless workflow in industrial settings. Additionally, the use of corrosion-resistant materials in the conveying line ensures long-term durability and reduces maintenance costs.
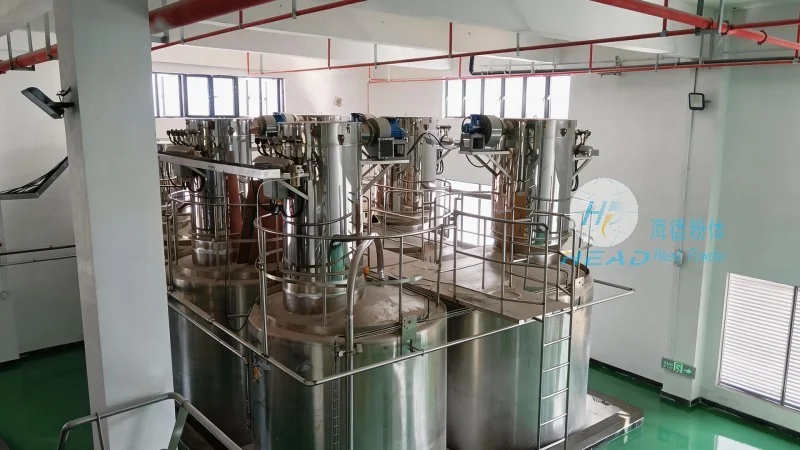
Caustic soda pneumatic conveying systems are widely used across various industries that rely on caustic soda in their production processes. These include the pulp and paper industry, where caustic soda is used for pulp digestion and bleaching; the chemical industry, for manufacturing other chemicals and cleaning agents; the textile industry, for processing fibers and fabrics; and the food industry, for certain food processing applications. The versatility of the system makes it suitable for handling different forms of caustic soda, such as solid flakes, pellets, or granules, depending on the specific requirements of the application.
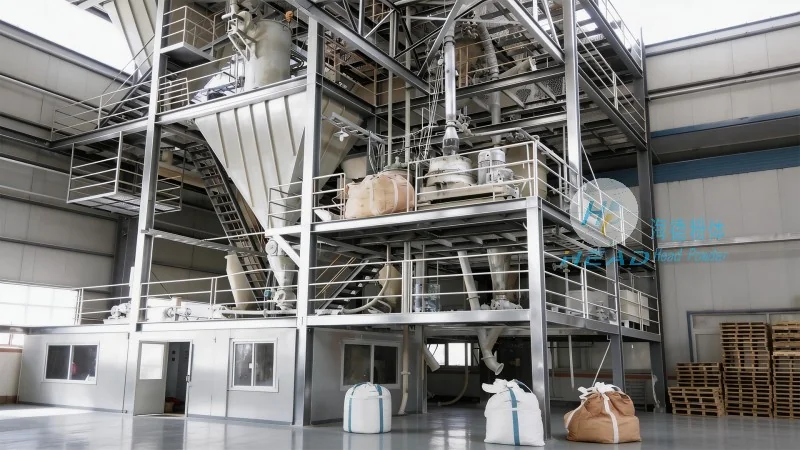
While pneumatic conveying systems offer many benefits, proper operation and safety measures are essential to ensure their effectiveness and protect personnel. Regular maintenance of the blower, feeder, and conveying line is crucial to prevent breakdowns and ensure consistent performance. The system should be designed with appropriate safety features, such as pressure relief valves and dust collection systems, to mitigate any potential risks. Additionally, operators should be trained on the proper handling of caustic soda and the operation of the conveying system to avoid accidents. Compliance with local regulations and industry standards is also important to ensure the system meets all safety and environmental requirements.
In conclusion, caustic soda pneumatic conveying systems are an efficient and safe solution for transporting caustic soda in industrial settings. By understanding the fundamental principles and components of these systems, industries can make informed decisions about implementing or upgrading their material handling processes. The benefits of enclosed transport, energy efficiency, and integration with other equipment make pneumatic conveying a preferred choice for many applications. As technology advances, further improvements in system design and materials may enhance the performance and reliability of caustic soda pneumatic conveying systems, contributing to better operational outcomes and safety in industrial environments.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top