Ammonium sulfate, a widely used industrial chemical, often requires efficient and reliable transportation methods to ensure smooth production processes. Pneumatic conveying equipment has emerged as a critical solution for handling such powders, offering advantages in terms of safety, cleanliness, and operational flexibility. This article delves into the specifics of ammonium sulfate pneumatic conveying equipment, exploring its structure, working principles, and the key components that enable effective powder transport.
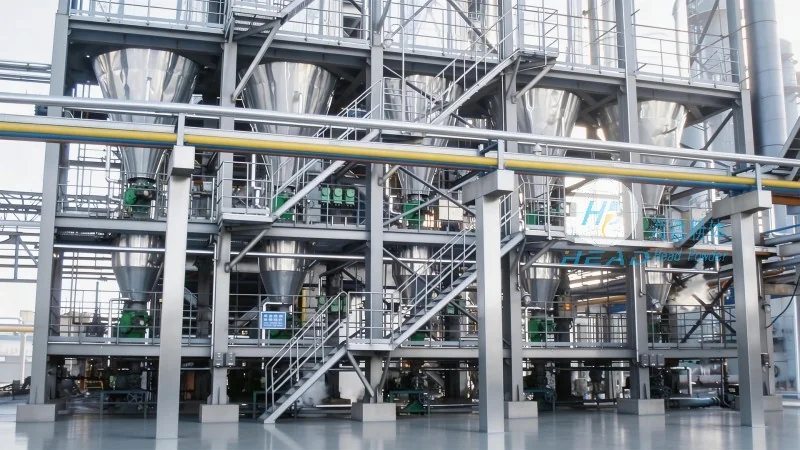
The foundation of any pneumatic conveying system lies in its integrated components, each playing a vital role in the efficient movement of ammonium sulfate. A typical system consists of several key elements, including the feed hopper, air compressor, conveying pipeline, and separation unit. The feed hopper is designed to store and meter the ammonium sulfate, ensuring a consistent flow into the system. This component often incorporates a rotary valve or a screw feeder to control the material discharge rate, preventing overloading and maintaining system stability.
Next, the air compressor generates the necessary air pressure to create the conveying medium. This compressed air is then directed into the conveying pipeline, where it interacts with the ammonium sulfate particles. The pipeline itself is constructed from materials resistant to corrosion and abrasion, such as stainless steel or special plastic composites, to withstand the chemical properties of ammonium sulfate and the wear from repeated particle movement.
The separation unit is a critical component for completing the conveying process. As the mixture of air and powder reaches the end of the pipeline, it enters the separator, where the air and solid particles are separated. This separation can be achieved through various mechanisms, including cyclone separators or bag filters, depending on the system design. The separated air is then typically vented, while the ammonium sulfate is collected in a receiving hopper or storage tank.
The operation of an ammonium sulfate pneumatic conveying system is based on the principle of creating a low-pressure or high-pressure air stream to transport the powder. In a typical low-pressure system, the air compressor provides a relatively low pressure (usually 0.5 to 1 bar) to move the material through the pipeline. The powder is suspended in the air stream, and the velocity of the air ensures that the particles remain airborne, preventing blockages and ensuring smooth transport.
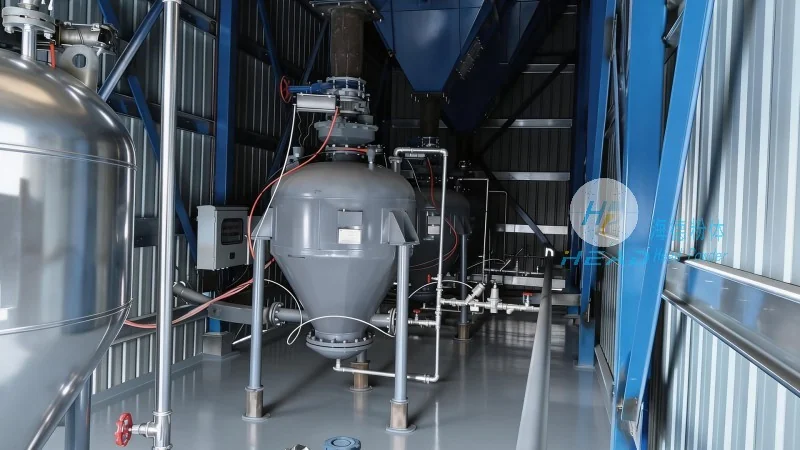
High-pressure systems, on the other hand, operate at higher pressures (up to 10 bar or more) and are often used for longer distances or more challenging material characteristics. The increased pressure allows for more efficient particle suspension and reduces the risk of particle deposition in the pipeline. The choice between low-pressure and high-pressure systems depends on factors such as the distance to be covered, the material's flow properties, and the desired system efficiency.
During the conveying process, the air and powder mixture travels through the pipeline at a velocity sufficient to keep the particles in suspension. The design of the pipeline, including bends and fittings, is carefully engineered to minimize pressure losses and maintain the air velocity required for effective transport. Properly sized and positioned components, such as expansion joints and flow straighteners, help to ensure consistent air flow and prevent turbulence that could lead to particle deposition.
Implementing pneumatic conveying for ammonium sulfate offers several advantages over traditional methods like belt conveyors or bucket elevators. One of the primary benefits is the elimination of direct human contact with the material, enhancing workplace safety. Pneumatic systems also provide a cleaner and more hygienic environment, as the material is transported within enclosed pipelines, reducing dust and contamination risks.
Another key advantage is the flexibility of pneumatic conveying systems. They can be easily adapted to different production layouts, allowing for changes in the material flow path without significant modifications to the infrastructure. This adaptability is particularly valuable in industries where production processes may evolve or where space constraints are a factor.
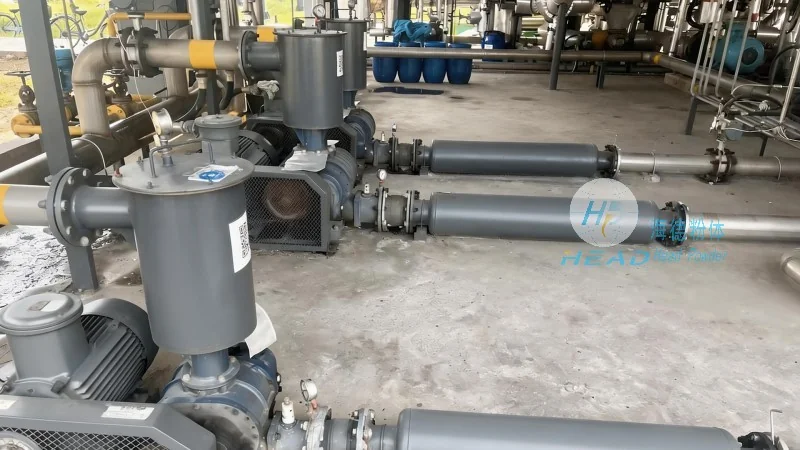
Efficiency is also a significant benefit. Pneumatic systems can transport materials over longer distances with less energy consumption compared to mechanical conveyors, especially when operating at high pressures. The ability to handle a wide range of particle sizes and flow rates makes these systems versatile for various applications, including bulk handling in chemical and fertilizer industries.
Ammonium sulfate pneumatic conveying equipment is widely used in the chemical, fertilizer, and food processing industries. In the chemical sector, it is essential for transporting raw materials and finished products, ensuring that production lines operate continuously without interruptions. The fertilizer industry, in particular, relies heavily on these systems to move ammonium sulfate, a key component in nitrogen-based fertilizers, from storage to processing facilities.
The food processing industry also benefits from the use of pneumatic conveying systems, as they help maintain the quality and safety of powdered products. By keeping the material enclosed and preventing contamination, these systems ensure that the final products meet regulatory standards and consumer expectations.
Moreover, the use of pneumatic conveying in these industries contributes to improved operational efficiency and reduced downtime. By minimizing material handling errors and ensuring consistent flow rates, companies can enhance their overall productivity and profitability.
When selecting a pneumatic conveying system for ammonium sulfate, several factors must be considered to ensure optimal performance and longevity. The first consideration is the material's physical properties, such as particle size, density, and moisture content. These characteristics influence the system's design, including the choice of air pressure, pipeline diameter, and separation technology.
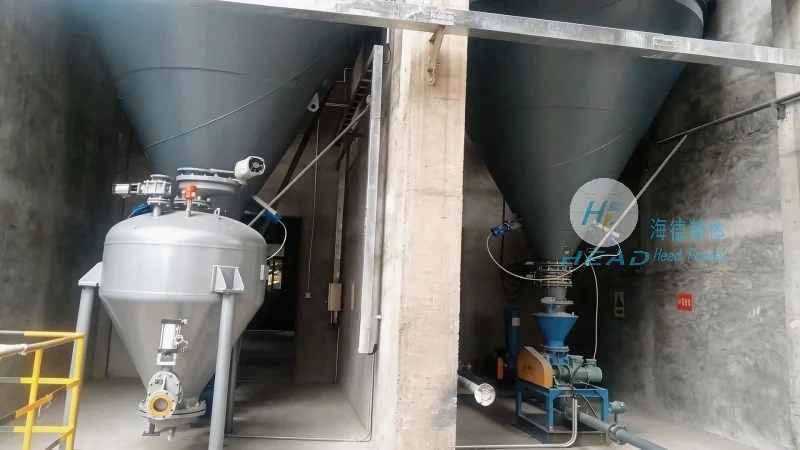
System capacity is another critical factor. The required throughput, measured in tons per hour, determines the size of the air compressor and the diameter of the conveying pipeline. Proper sizing ensures that the system can handle the intended production volume without excessive energy consumption or pressure losses.
Corrosion resistance is also a key consideration, as ammonium sulfate can be corrosive to certain materials. Materials like stainless steel or specialized coatings are often used for components that come into direct contact with the material to prevent degradation and maintain system integrity.
Installation and maintenance requirements are additional factors to evaluate. Pneumatic systems require regular maintenance, including cleaning of the separation unit and checking the air compressor for efficiency. Proper maintenance schedules help to extend the system's lifespan and minimize operational disruptions.
Ammonium sulfate pneumatic conveying equipment represents a sophisticated solution for the efficient and safe transport of powders in industrial settings. By understanding the structure and working principles of these systems, as well as the key considerations for implementation, companies can make informed decisions that enhance their operational efficiency and product quality. The use of such equipment not only improves the handling of ammonium sulfate but also contributes to a safer and more sustainable industrial environment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top