Bentonite, a versatile clay widely used in various industrial applications, often requires efficient and reliable handling methods to ensure optimal performance. Pneumatic conveying equipment has emerged as a critical solution for transporting bentonite and other fine powders, offering advantages such as dust-free operation, flexibility in layout, and the ability to handle sensitive materials without degradation. This article delves into the components, working principles, and practical applications of bentonite pneumatic conveying systems, providing a comprehensive overview for industry professionals seeking to understand or implement such technology.
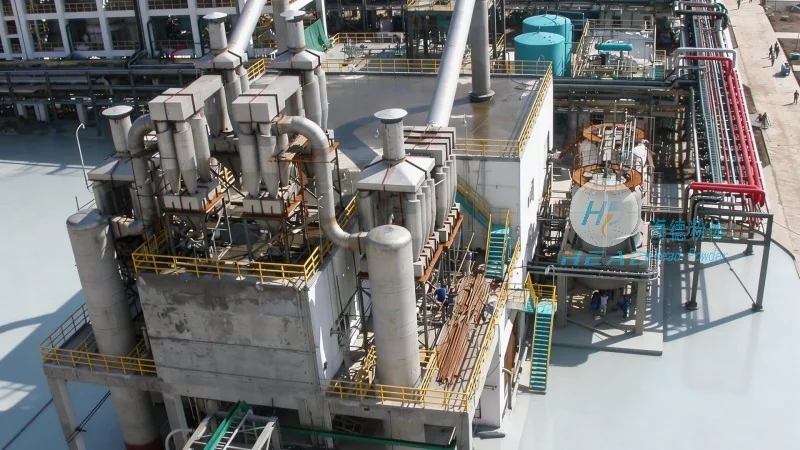
At the heart of any bentonite pneumatic conveying system lies a series of interconnected components designed to move material from the source to the destination while maintaining efficiency and safety. The primary components typically include a material feed hopper, a conveying line (either rigid or flexible), a dust separator, and a collection bin. Each component plays a vital role in the overall operation, and their design directly impacts the system's performance and reliability.
The material feed hopper is responsible for storing and feeding the bentonite powder into the conveying line. It often features a hopper with a sloped bottom to facilitate smooth material flow, equipped with a rotary valve or feeder to control the discharge rate. This component ensures a consistent feed rate, preventing blockages and maintaining system stability. The conveying line, which can be made of metal or flexible tubing, is where the material is propelled by air pressure. The choice between positive pressure (air blowing material) and negative pressure (suction) depends on the application requirements, material characteristics, and system layout.
The dust separator, a critical component for maintaining air quality and preventing material loss, is typically located at the end of the conveying line. It works by reducing the air velocity, allowing the bentonite particles to settle out and be collected in the hopper. Common types of separators include cyclone separators, bag filters, and electrostatic precipitators, each offering different levels of efficiency and maintenance requirements. Finally, the collection bin stores the conveyed bentonite, providing a buffer for downstream processing or storage. Some systems may also include a vacuum pump or blower to generate the necessary air pressure for positive or negative pressure conveying.
The operational principle of bentonite pneumatic conveying systems revolves around the use of air to transport fine powders. In positive pressure systems, a blower or compressor generates high-pressure air that is introduced into the conveying line, pushing the bentonite particles forward. The air velocity must be sufficient to overcome the gravitational force and friction within the line, ensuring the material remains suspended and moves efficiently. Conversely, negative pressure systems use a vacuum pump to create a low-pressure environment, drawing the bentonite particles into the line as they are pulled toward the source. Both methods rely on the principle of fluidization, where the air flow creates a suspension of the powder particles, allowing them to be transported without direct contact with the conveying line.
Key factors influencing the efficiency of pneumatic conveying include the air velocity, material properties (such as particle size, density, and moisture content), and system design. For bentonite, which is often a fine, cohesive powder, maintaining an appropriate air velocity is crucial to prevent clogging and ensure uniform flow. The system must also account for the material's tendency to stick to surfaces, requiring anti-static coatings or lubricants in some cases to reduce friction and improve material release.
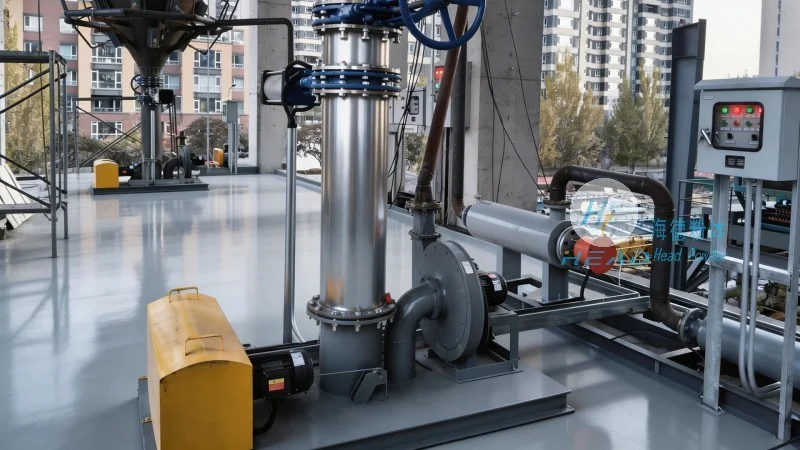
Another important aspect of the working principle is the control of air pressure and flow rate. Modern systems often incorporate variable frequency drives (VFDs) to adjust the blower speed, allowing for precise control over the conveying rate. This flexibility enables operators to match the system's output to the processing requirements, optimizing energy consumption and material handling efficiency. Additionally, the use of sensors and monitoring systems helps in real-time tracking of material flow, pressure, and air quality, facilitating proactive maintenance and troubleshooting.
Bentonite pneumatic conveying systems find extensive applications across various industries, including pharmaceuticals, food processing, and construction. In the pharmaceutical industry, for example, these systems are used to transport bentonite as a filler or excipient, requiring strict contamination control and dust-free operation. The ability to handle fine powders without particle degradation makes pneumatic conveying ideal for sensitive applications where material quality is paramount. In the food industry, similar requirements apply, with the added need for hygienic design and compliance with food safety regulations.
In the construction sector, bentonite is commonly used as a sealant or stabilizer in geotechnical applications. Pneumatic conveying allows for the efficient transport of bentonite from storage to mixing sites, ensuring consistent material delivery and reducing manual handling risks. The benefits of using pneumatic conveying in these applications include improved safety, reduced labor costs, and enhanced product quality due to minimal material exposure to contaminants.
From an operational perspective, bentonite pneumatic conveying offers several advantages over traditional methods such as belt conveyors or bucket elevators. One of the most significant benefits is the elimination of dust and the associated health hazards, as the material is contained within the conveying line. This not only improves workplace safety but also reduces the need for dust control measures, such as filtration systems or ventilation. Additionally, pneumatic systems can be designed to handle long distances and complex layouts, making them suitable for large-scale industrial facilities where material transport is a critical operation.
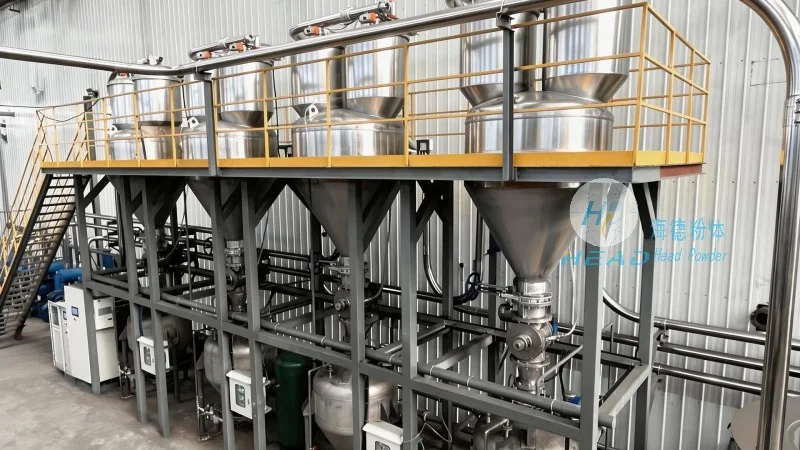
Energy efficiency is another key advantage of modern bentonite pneumatic conveying systems. Advances in blower technology and system design have led to more energy-efficient operations, reducing operational costs and environmental impact. The ability to adjust air pressure and flow rate according to demand further optimizes energy consumption, making these systems a cost-effective solution for long-term material handling needs.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of powder handling equipment, specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to the needs of various industries. With a strong focus on innovation and quality, the company has built a reputation for delivering reliable and efficient solutions for handling fine powders, including bentonite. HeadPowder's expertise lies in understanding the unique challenges of material transport and providing customized solutions that meet the specific requirements of each client.
HeadPowder's manufacturing facility, located in Shandong, China, is equipped with state-of-the-art equipment and adheres to strict quality control standards. The company's team of engineers and technicians brings extensive experience in powder technology, ensuring that each product is designed to meet the highest performance and safety standards. From initial consultation and system design to installation and after-sales support, HeadPowder provides comprehensive services to ensure client satisfaction and long-term operational success.
The company's commitment to customer service and technical support is evident in its approach to addressing client needs. By working closely with clients to understand their operational requirements and challenges, HeadPowder develops tailored solutions that enhance productivity and reduce costs. This collaborative approach has helped the company build a strong client base and maintain a competitive edge in the market.
With a focus on sustainability and environmental responsibility, HeadPowder also incorporates eco-friendly design principles into its products. This includes the use of energy-efficient components, dust control measures, and materials that minimize environmental impact. By prioritizing both performance and sustainability, HeadPowder aims to contribute to the development of more efficient and responsible industrial practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top