Water-containing powder pneumatic conveying systems are sophisticated industrial solutions designed to transport powders and granular materials through a pressurized or vacuum air stream. These systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and manufacturing, due to their efficiency and ability to handle sensitive materials. The core components of such a system are essential for ensuring reliable and safe operation, and understanding each part is crucial for optimal performance and maintenance.
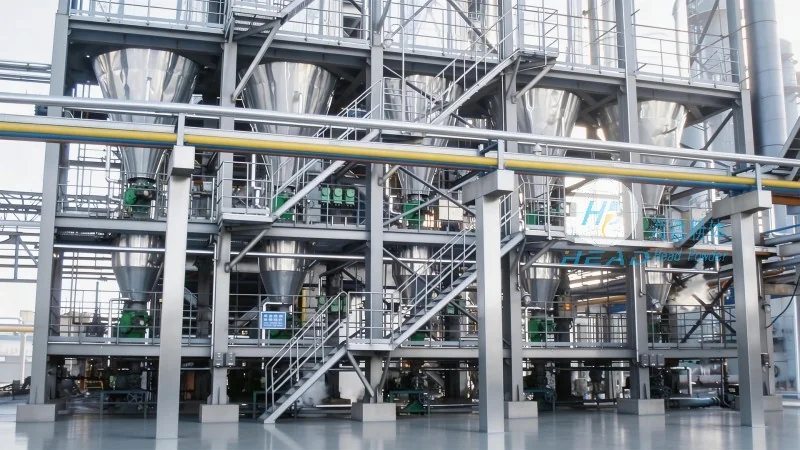
The water-containing powder pneumatic conveying system typically consists of several critical components that work in tandem to achieve the desired material transport. These components are engineered to handle the unique challenges posed by powders, such as dust generation, caking, and moisture sensitivity. The primary components include:
The material hopper is the initial storage unit where the powder or granular material is held before it is conveyed. It is designed to accommodate the bulk of the material and ensure a consistent feed rate. The feeder, often a rotary valve or a screw feeder, regulates the flow of material from the hopper into the conveying line. This component is critical for maintaining a steady supply of material to the system, preventing blockages and ensuring smooth operation. The design of the hopper and feeder must consider factors like material density, flowability, and potential for agglomeration, especially when dealing with water-containing powders that may have higher moisture content. The hopper is typically constructed from corrosion-resistant materials such as stainless steel or high-density polyethylene to withstand the effects of moisture and chemical exposure. Its shape and dimensions are optimized to minimize material bridging and prevent the formation of clumps, which can disrupt the conveying process. The feeder is equipped with adjustable speed controls to match the system's requirements, allowing for precise regulation of the material flow rate. For water-containing powders, the feeder may incorporate heating elements or anti-caking agents to maintain the material's flowability and prevent blockages caused by moisture-induced agglomeration.
The conveying line, typically made of stainless steel or other corrosion-resistant materials, forms the pathway for the material and air mixture. The tubing is designed to withstand the pressure and temperature conditions of the system and to minimize friction losses. The diameter and length of the line are carefully selected based on the material characteristics, conveying distance, and desired flow rate. For water-containing powders, the tubing may need to be equipped with special features, such as anti-corrosion coatings or internal linings, to prevent degradation from moisture and chemical interactions. The line is usually connected to the system using fittings and joints that are sealed to maintain the system's pressure integrity. The material of the tubing, often 316L stainless steel, is chosen for its resistance to corrosion and its ability to handle the moisture-laden air and powder mixture. The line's diameter is determined by the material's particle size and flow rate requirements, ensuring that the air velocity is sufficient to prevent material settling but not excessive enough to cause excessive pressure drops or wear on the system components.
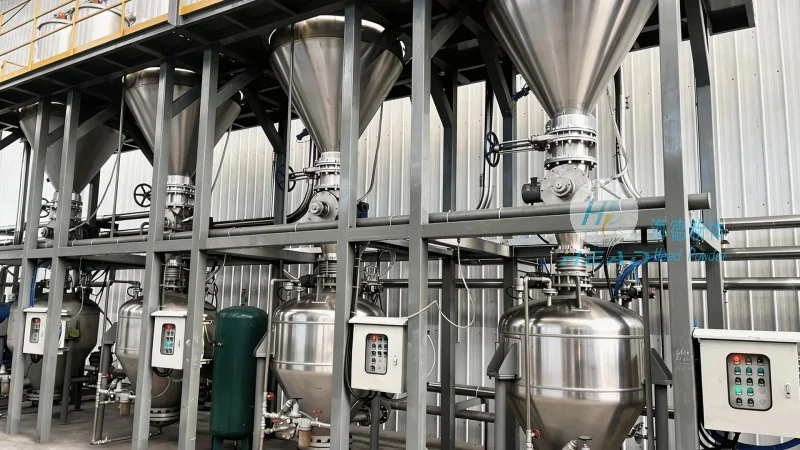
The air supply system, including a compressor and associated equipment, provides the necessary pressure or vacuum to move the material through the conveying line. The compressor generates the air pressure required to overcome the resistance in the line and to lift the material. The unit may include components like air filters, regulators, and moisture separators to ensure the air quality is suitable for the material being conveyed. For water-containing powders, the air supply must be dry and free of contaminants to prevent moisture from affecting the material's properties or causing corrosion in the system components. The compressor's capacity and efficiency are critical factors that impact the system's overall performance and energy consumption. The compressor is typically a positive displacement type, such as a rotary screw or reciprocating compressor, which can deliver the required pressure and flow rate. The air filter removes particulate matter and moisture from the air, while the regulator maintains a stable pressure level. The moisture separator further removes any residual water vapor to ensure the air is dry enough for the material.
A key feature of water-containing powder pneumatic conveying is the integration of water into the system. The water injection system is responsible for adding the appropriate amount of water to the powder stream, which helps to improve flowability, reduce dust, and enhance the overall conveying efficiency. The system typically includes a water pump, a metering device, and a nozzle or spray system that injects the water into the conveying line at the correct location. The mixing process is crucial for achieving a uniform blend of powder and water, which ensures consistent performance throughout the conveying process. The water injection rate is carefully controlled based on the material's moisture content and the desired conveying characteristics. This component is essential for optimizing the system's performance, especially when dealing with materials that are prone to caking or have low flowability. The water pump is usually a centrifugal type, capable of delivering the required flow rate and pressure. The metering device, such as a flow meter or a mass flow controller, ensures precise control over the water addition. The nozzle or spray system is positioned in the conveying line to ensure the water is evenly distributed with the powder, preventing localized wetting that could lead to uneven flow or blockages.
The control and monitoring system manages the operation of the entire water-containing powder pneumatic conveying system. It includes sensors, controllers, and indicators that monitor parameters such as pressure, flow rate, temperature, and moisture content. The system may also include automated controls that adjust the feeder speed, water injection rate, or air pressure based on real-time feedback. This allows for precise control over the conveying process and helps to prevent issues like overloading or under-conveying. The monitoring equipment is vital for maintaining the system's efficiency and for early detection of potential problems, such as blockages or equipment failures. Regular maintenance and calibration of these components are necessary to ensure reliable operation. The control system may be a programmable logic controller (PLC) or a distributed control system (DCS), which provides centralized monitoring and control of all system parameters. The sensors, including pressure transducers, flow meters, and temperature sensors, provide real-time data to the controller, which then adjusts the system settings as needed. The indicators, such as alarms and displays, alert operators to any deviations from the normal operating conditions, allowing for timely intervention and problem resolution.
Due to the nature of powders, dust generation is a common issue in pneumatic conveying systems. The dust collection and filtration system is designed to capture and remove airborne particles, ensuring a clean and safe working environment. This system typically includes a dust collector, filter bags or cartridges, and a fan or blower to draw air through the filtration media. The collected dust is then disposed of or recycled, depending on the material's properties and regulatory requirements. For water-containing powders, the filtration system may need to be equipped with special filters to handle moisture-laden air and to prevent clogging. The design of the dust collection system is critical for maintaining air quality and complying with environmental regulations. Proper maintenance of the filters is essential to prevent pressure drops and ensure the system operates efficiently. The dust collector is usually a baghouse or a cartridge filter, which can handle high volumes of air and capture fine particles. The fan or blower provides the necessary airflow to pass the air through the filtration media, and the collected dust is removed from the filter bags or cartridges through a shaking or pulse-jet system. The system is designed to maintain a consistent pressure drop across the filters, indicating when cleaning or replacement is required. For water-containing powders, the filters may be equipped with moisture-resistant materials or anti-caking coatings to prevent clogging from moisture-laden dust.
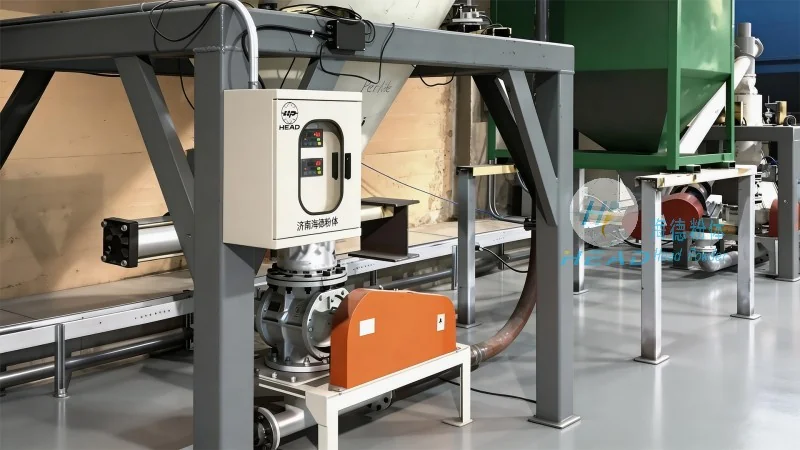
The discharge equipment is responsible for delivering the conveyed material to its final destination. This may include a receiving hopper, a silo, or a processing unit. The design of the discharge system must ensure that the material is deposited without causing spillage or blockages. For water-containing powders, the discharge equipment may need to be equipped with features like anti-caking mechanisms or moisture control to prevent material degradation. The collection equipment is typically integrated with the dust collection system to ensure that any residual dust is captured before it is released into the environment. The discharge and collection components are crucial for completing the material transport process and ensuring that the material is handled safely and efficiently. The receiving hopper or silo is designed to store the conveyed material and maintain a consistent level, preventing overfilling or underfilling. The discharge valve, such as a rotary valve or a gate valve, controls the flow of material from the hopper to the processing unit. For water-containing powders, the discharge equipment may incorporate heating elements or anti-caking agents to maintain the material's flowability and prevent blockages caused by moisture-induced agglomeration. The collection system may include a hopper or a bag for collecting the material, which can then be disposed of or recycled. The design of the discharge and collection equipment ensures that the material is handled in a clean and safe manner, minimizing the risk of contamination or spillage.
Water-containing powder pneumatic conveying systems require additional safety and maintenance components to ensure safe and reliable operation. These components include pressure relief valves, safety interlocks, and maintenance access points. The pressure relief valve is installed to protect the system from overpressure conditions, which can occur due to blockages or equipment failures. The safety interlocks are designed to stop the system in the event of an emergency, such as a power failure or a pressure drop. The maintenance access points allow for easy inspection and repair of the system components. Regular maintenance of these components is essential to ensure the system operates safely and efficiently. The pressure relief valve is typically set to a pressure slightly above the normal operating pressure, ensuring that it activates only in case of an emergency. The safety interlocks are integrated with the control system to automatically shut down the system if a safety condition is detected. The maintenance access points are strategically placed to allow for easy access to the hopper, feeder, and other components, facilitating routine inspections and repairs. The system may also include a maintenance schedule that outlines the frequency of inspections and repairs, ensuring that the system is maintained in optimal condition.
The components and systems described above are typically supplied by specialized engineering companies that design and manufacture pneumatic conveying solutions. One such company is Shandong HeadPowder Engineering Co., Ltd., a leading provider of water-containing powder pneumatic conveying systems. The company is based in Shandong, China, and has extensive experience in designing and implementing systems for various industries. HeadPowder offers a range of components and systems tailored to the specific needs of its clients, ensuring that the systems are reliable, efficient, and safe. The company's expertise in material handling and pneumatic conveying technology allows it to provide customized solutions that meet the unique requirements of each application. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for many businesses in need of effective powder conveying solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top