Pharmaceutical particle conveyance is a critical process in the manufacturing and handling of medicinal products. The efficiency and reliability of the system directly impact product quality, safety, and operational costs. Among the various technologies available, air-driven structures have emerged as a preferred solution due to their ability to handle sensitive materials while maintaining high levels of hygiene and contamination control. This article explores the main air-driven structures used in pharmaceutical particle conveyance, highlighting their applications and benefits.
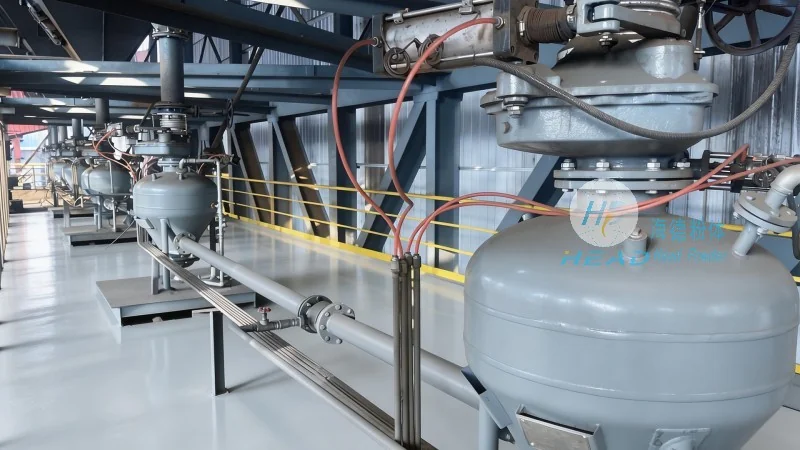
Before delving into specific structures, it is essential to understand the fundamental principles of air-driven conveyance. These systems utilize air pressure or vacuum to transport bulk materials, such as pharmaceutical powders and granules, through pipelines. The choice of system depends on factors like material characteristics, process requirements, and environmental considerations. Air-driven conveyance offers advantages including minimal product degradation, reduced risk of cross-contamination, and the ability to operate in cleanroom environments.
Several air-driven structures are commonly employed in pharmaceutical manufacturing. Each has unique features and is suited to specific applications. The primary structures include positive pressure systems, negative pressure systems, and hybrid systems. These systems are designed to meet stringent regulatory standards, ensuring compliance with Good Manufacturing Practices (GMP) and other industry guidelines.
Positive pressure systems operate by blowing air into the conveying line, creating a pressure higher than the ambient environment. This method is particularly effective for transporting materials that are prone to dust generation or contamination. The system typically includes a blower, a material feed hopper, and a discharge point. The air flow carries the particles through the pipeline, ensuring a continuous and controlled flow. A key advantage of positive pressure systems is their ability to prevent external air from entering the system, thus maintaining a sterile and clean environment. This is crucial in pharmaceutical applications where product purity is paramount.
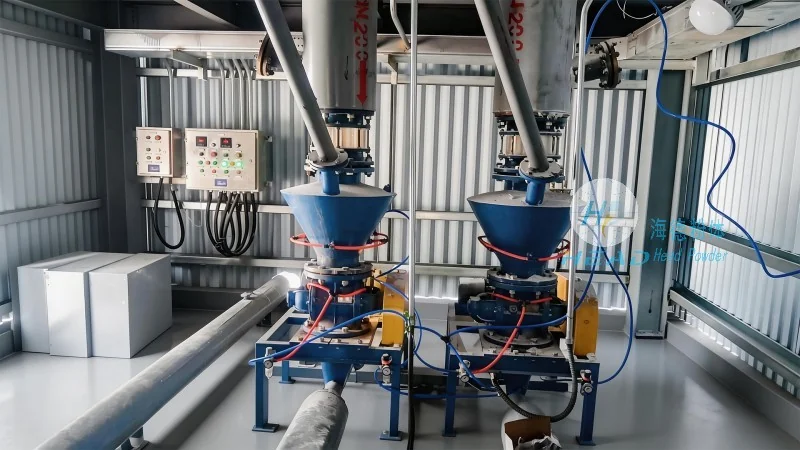
Negative pressure systems, also known as vacuum or suction systems, work by creating a vacuum inside the conveying line. The lower pressure draws material from the source into the pipeline. This approach is ideal for applications where the material needs to be drawn from a height or where the source is located in a confined space. The system consists of a vacuum pump, a material hopper, and a discharge point. The vacuum pulls the particles through the pipeline, ensuring efficient transport. Negative pressure systems are often preferred when dealing with materials that are lightweight or have low bulk density, as the suction force helps maintain a consistent flow.
Hybrid systems combine elements of both positive and negative pressure systems. They utilize a combination of pressure and vacuum to optimize material transport. For instance, a hybrid system might use a positive pressure blower to move material from the source to a central point and then switch to a negative pressure suction to transport it to the final destination. This approach allows for greater flexibility and efficiency, especially in complex manufacturing processes where materials need to be transported over long distances or through multiple stages. Hybrid systems are particularly useful in pharmaceutical production lines that involve multiple processing steps and require precise control over material flow.
The effectiveness of air-driven structures in pharmaceutical particle conveyance is enhanced by proper material handling and process integration. This includes the use of appropriate hopper designs to prevent material bridging and agglomeration, which can disrupt the flow. Additionally, the selection of pipeline materials, such as stainless steel or PTFE-coated tubing, is critical to maintain product integrity and prevent contamination. The integration of sensors and control systems allows for real-time monitoring of the conveying process, ensuring that any deviations are immediately detected and corrected. This level of control is essential for maintaining consistent product quality and meeting regulatory requirements.
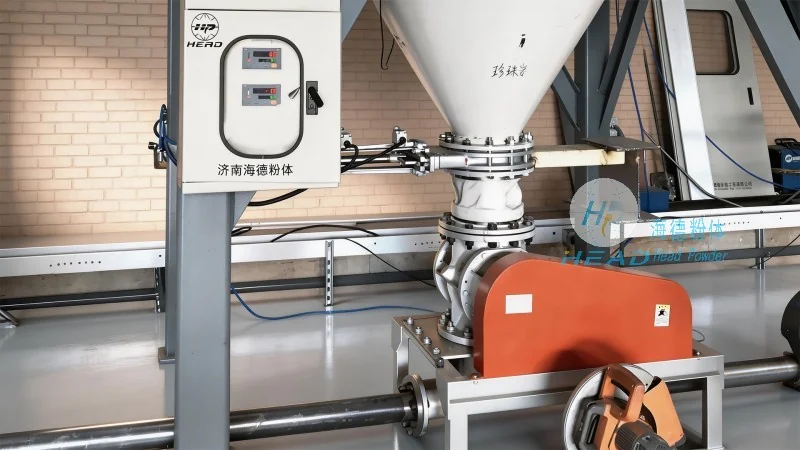
Pharmaceutical manufacturing is subject to stringent regulatory standards, and air-driven conveyance systems must comply with these guidelines. The systems are designed to meet Good Manufacturing Practices (GMP), which emphasize cleanliness, safety, and product quality. Components such as blower housings, hopper liners, and pipeline connections are constructed from materials that are easy to clean and sanitize. The use of air filtration systems, such as HEPA filters, ensures that the air used in the conveying process is free from contaminants. Regular maintenance and inspection of the system are also required to ensure ongoing compliance with regulatory standards. These measures help to minimize the risk of product contamination and ensure that the final pharmaceutical products meet the required quality standards.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pharmaceutical processing solutions, has successfully implemented air-driven conveyance systems in various pharmaceutical manufacturing facilities. The company specializes in designing and manufacturing customized air-driven structures tailored to the specific needs of clients. For example, a client required a system to transport sensitive granules from a mixing tank to a packaging line. HeadPowder designed a positive pressure system with a stainless steel hopper and a HEPA-filtered blower. The system was integrated with the client's existing process, ensuring seamless operation and compliance with GMP standards. The result was improved material flow, reduced downtime, and enhanced product quality. This case study illustrates the effectiveness of air-driven structures in real-world pharmaceutical applications and highlights the expertise of HeadPowder in providing tailored solutions.
Air-driven structures play a vital role in pharmaceutical particle conveyance, offering efficient, hygienic, and reliable transport of bulk materials. The main structures, including positive pressure, negative pressure, and hybrid systems, each have unique advantages and are selected based on specific process requirements. Proper material handling, process integration, and adherence to regulatory standards are essential for maximizing the benefits of these systems. Companies like Shandong HeadPowder Engineering Co., Ltd. continue to innovate and provide advanced air-driven solutions that meet the evolving needs of the pharmaceutical industry. By leveraging these technologies, manufacturers can enhance productivity, ensure product quality, and maintain compliance with industry regulations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top