Headpowder, a leading engineering firm based in Shandong, China, specializes in providing comprehensive turnkey solutions for sulfur pellet pneumatic conveying systems. This article explores the key aspects of such projects, highlighting the technical innovations, operational benefits, and practical applications that define modern sulfur handling infrastructure.
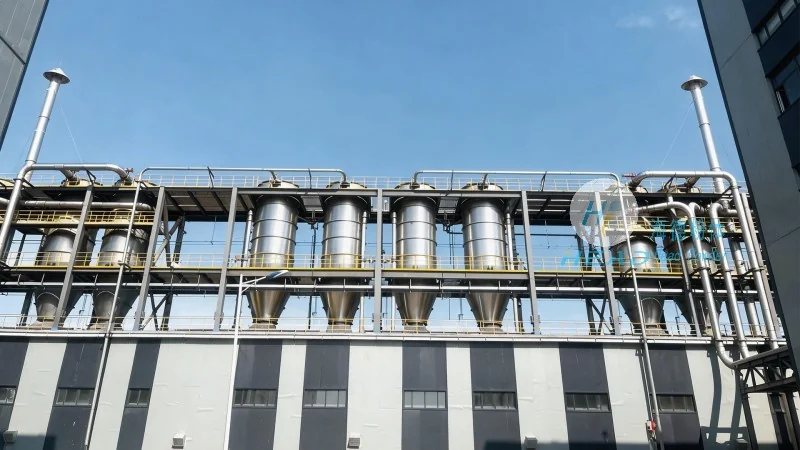
Sulfur pellets are a critical raw material in various industrial processes, including the production of sulfuric acid, fertilizers, and other chemical compounds. Efficient and reliable transportation of these pellets from storage to processing units is essential for maintaining production continuity and optimizing operational costs. Pneumatic conveying systems offer a superior alternative to traditional methods like belt conveyors or bucket elevators, providing advantages such as reduced dust generation, lower maintenance requirements, and enhanced safety in handling potentially hazardous materials like sulfur.
A turnkey project for sulfur pellet pneumatic conveying involves the design, procurement, installation, and commissioning of a complete system tailored to the client's specific needs. The core components typically include:
1. Suction and Discharge Units: These are the primary devices responsible for creating the airflow and transporting the pellets. Suction units draw the material from the storage silo, while discharge units deliver it to the processing equipment. The design of these units is critical, as they must handle the specific characteristics of sulfur pellets, including their density, size, and flowability.
2. Air Handling Equipment: This includes blowers, fans, and filters that generate the necessary air pressure and ensure clean, dry air for conveying. The selection of air handling equipment is based on the system's capacity, the distance of material transport, and the required air velocity to achieve efficient pellet movement.
3. Piping and Fittings: The system's piping network connects all components and ensures the smooth flow of both pellets and air. High-quality materials like stainless steel or corrosion-resistant alloys are used to prevent material degradation and system failure due to chemical exposure.
4. Control Systems: Advanced control systems monitor and regulate the operation of the pneumatic conveying system, ensuring optimal performance and safety. These systems can include sensors for pressure, flow, and temperature, as well as automated controls for start-up, shutdown, and emergency situations.
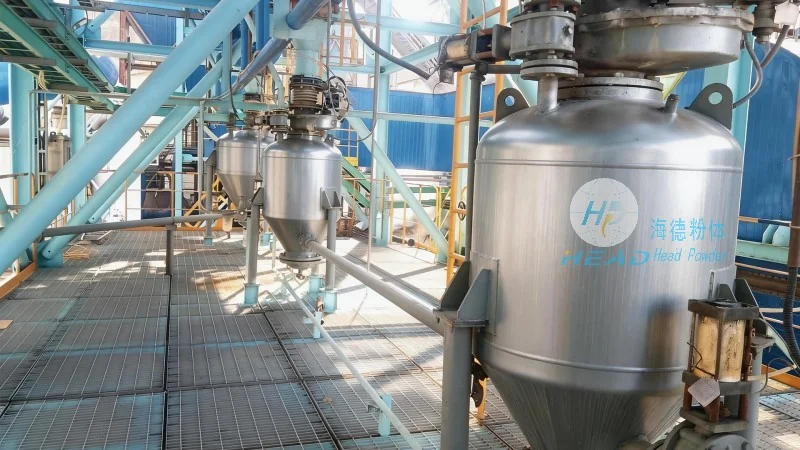
Compared to other material handling methods, pneumatic conveying offers several distinct advantages for sulfur pellet transport:
Firstly, minimal dust generation is a significant benefit. Unlike mechanical systems that can cause dust through friction or impact, pneumatic conveying uses enclosed pipes, reducing the risk of dust exposure and improving workplace safety. This is particularly important in industries where dust can be a health hazard or cause environmental contamination.
Secondly, flexibility in layout is another key advantage. Pneumatic systems can be easily reconfigured or expanded to accommodate changes in production requirements or facility expansions. The ability to route material vertically, horizontally, or at angles makes them suitable for complex plant layouts.
Thirdly, lower maintenance costs are achieved due to the reduced number of moving parts compared to mechanical conveyors. Mechanical systems often require regular lubrication, part replacement, and alignment checks, which can be time-consuming and costly. Pneumatic systems, with their simpler design, require less maintenance and have longer service lives.
Fourthly, enhanced safety is a critical consideration when handling sulfur pellets. Pneumatic conveying systems are enclosed, preventing accidental spills or exposure to the material. Additionally, the systems can be equipped with safety features such as pressure relief valves and emergency shutdown mechanisms to prevent accidents.
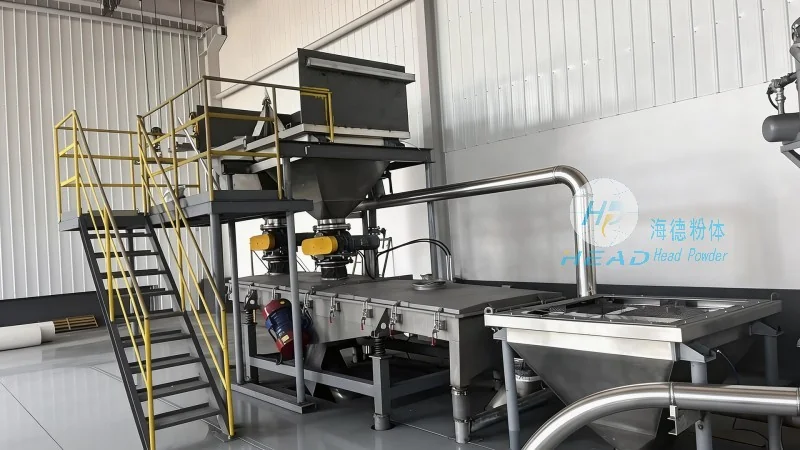
Sulfur pellet pneumatic conveying systems are widely used in various industrial applications. For instance, in the production of sulfuric acid, sulfur pellets are conveyed from storage silos to reactors or conversion units. In fertilizer manufacturing, the pellets are transported to mixing and granulation processes. In chemical processing plants, the material is used as a raw ingredient in the production of various chemicals.
Headpowder has successfully implemented numerous turnkey projects for sulfur pellet pneumatic conveying across different industries. One notable case involved a large-scale sulfuric acid plant in Shandong, where the company designed and installed a system capable of transporting 500 tons of sulfur pellets per hour. The system was customized to handle the specific challenges of the plant, including the need for high air pressure and the prevention of dust accumulation in the piping network.
Another successful project was for a fertilizer manufacturer, where Headpowder provided a pneumatic conveying system that integrated with existing storage and processing equipment. The system was designed to improve material flow efficiency and reduce downtime, resulting in significant cost savings for the client.
At Headpowder, we understand that every industrial facility has unique requirements. Therefore, our turnkey projects are fully customizable to meet the specific needs of our clients. We work closely with our clients to understand their operational goals, material characteristics, and facility constraints to design a system that is both efficient and cost-effective.
Our services include not only the design and installation of the pneumatic conveying system but also integration with existing infrastructure. This ensures a seamless transition from the old system to the new one, minimizing disruption to production. We also provide comprehensive training to the client's staff on the operation and maintenance of the system, ensuring that they can maximize its performance and lifespan.
Sulfur pellet pneumatic conveying turnkey projects represent a sophisticated solution for efficient material handling in industrial applications. By leveraging advanced engineering and technology, these systems offer significant advantages over traditional methods, including improved safety, reduced maintenance costs, and enhanced operational flexibility. Headpowder, with its expertise and experience in the field, is committed to providing high-quality turnkey solutions that meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top