Classification and Application Analysis of Polytrifluorochloroethylene Pneumatic Conveying Systems
Release time:2026-09-14 10:49:05
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
Polytrifluorochloroethylene (PTFE) is a high-performance fluoropolymer known for its exceptional chemical resistance, thermal stability, and low friction properties. In industrial applications, PTFE-based pneumatic conveying systems are widely used to transport fine powders and granules, especially in environments where conventional materials may degrade or fail. These systems are engineered to handle materials that are sensitive to moisture, heat, or corrosive substances, making them ideal for industries such as pharmaceuticals, food processing, and chemical manufacturing. The expertise of Shandong HeadPowder Engineering Co., Ltd. (headpowder) has been instrumental in developing advanced PTFE pneumatic conveying solutions tailored to meet the diverse needs of modern industries.
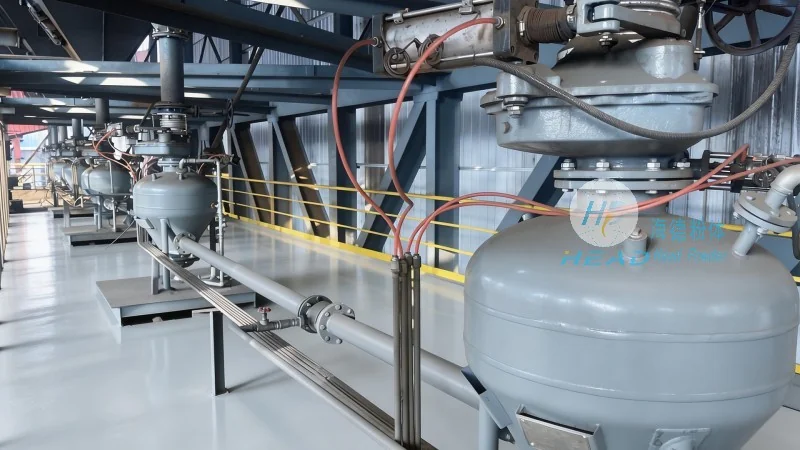
Classification of PTFE Pneumatic Conveying Systems
PTFE pneumatic conveying systems can be categorized based on several key factors, including the type of air flow, material handling capacity, and system design. The primary classifications include:
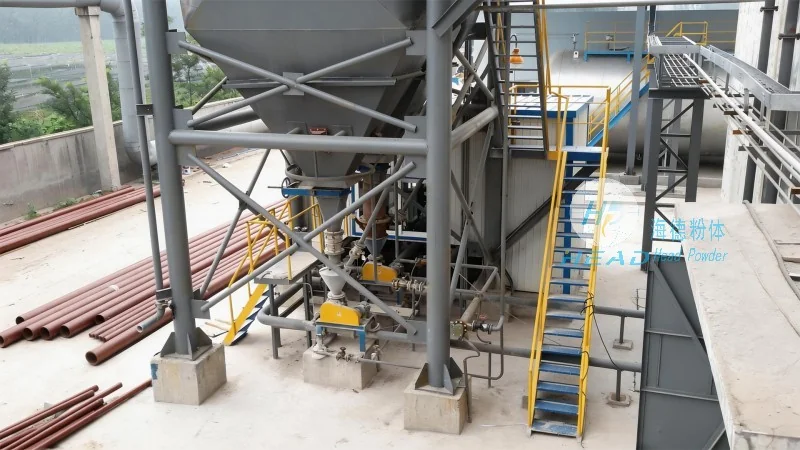
- Positive Pressure Systems: These systems use compressed air to push material through the conveying line. They are suitable for long-distance transport and can handle a wide range of particle sizes. Positive pressure systems are often preferred for applications requiring high material throughput and minimal product degradation.
- Negative Pressure (Vacuum) Systems: In these systems, a vacuum is created to draw material into the conveying line. They are ideal for applications where dust control is critical or where the material needs to be transported from multiple sources to a central collection point. Negative pressure systems are commonly used in environments where air quality must be maintained.
- Combined Pressure-Vacuum Systems: This hybrid approach combines elements of both positive and negative pressure systems. It allows for flexibility in material handling, enabling the system to switch between pushing and pulling material as needed. This type of system is particularly useful for complex conveying routes or when handling materials with varying properties.
Key Components of PTFE Pneumatic Conveying Systems
Regardless of the classification, PTFE pneumatic conveying systems typically consist of several core components. These include:
- Feeder: The feeder is responsible for accurately metering and feeding the material into the conveying line. For PTFE systems, feeders are often designed with special materials to prevent material buildup and ensure consistent flow.
- Conveying Line: The conveying line is the main pathway for transporting the material. In PTFE systems, the line is usually made from PTFE-coated or PTFE-lined components to provide corrosion resistance and reduce friction.
- Control Valves: Control valves regulate the air flow and pressure within the system, ensuring optimal material transport. These valves are critical for maintaining system efficiency and preventing material blockages.
- Receiver: The receiver is where the material is deposited after being conveyed. It is designed to handle the material's properties and prevent spillage or contamination.
- Filter and Dust Collector: To maintain air quality and comply with environmental regulations, PTFE systems often include a filter and dust collector. These components capture any fine particles that may be released during the conveying process.
Applications of PTFE Pneumatic Conveying Systems
PTFE pneumatic conveying systems find applications in a variety of industries due to their ability to handle challenging materials. Some common applications include:
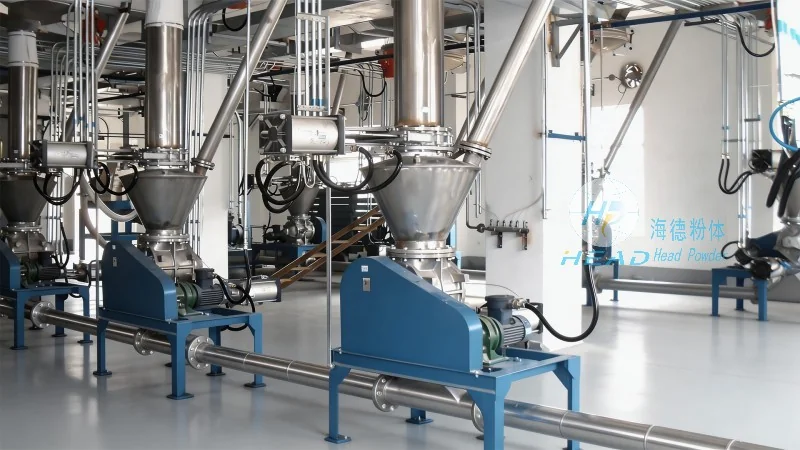
- Pharmaceutical Industry: In pharmaceutical manufacturing, PTFE systems are used to transport active pharmaceutical ingredients (APIs) and excipients. The systems' chemical resistance and low contamination risk make them suitable for producing high-purity products.
- Food and Beverage Industry: For food processing, PTFE systems are employed to handle sensitive food powders, such as spices, vitamins, and flavorings. The systems' non-stick and hygienic properties ensure that the food products remain uncontaminated and free from cross-contamination.
- Chemical Manufacturing: In chemical plants, PTFE systems are used to transport corrosive or reactive powders, such as catalysts and specialty chemicals. The systems' resistance to chemical attack and thermal stability prevent material degradation and equipment failure.
- Mineral and Mining Industry: PTFE systems are also used in the mineral processing sector to transport fine minerals and ores. The systems' ability to handle abrasive materials and maintain consistent flow is crucial for efficient production.
Advantages of PTFE Pneumatic Conveying Systems
PTFE pneumatic conveying systems offer several advantages over traditional material handling methods. These include:

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
