HeadPowder, a leading provider in the field of material handling solutions, specializes in dust pneumatic conveying systems. These systems are essential for efficiently transporting fine powders and granular materials over short to medium distances. The company, based in Shandong, China, offers a range of technologies tailored to meet diverse industrial needs. This article explores the various types of dust pneumatic conveying, their key characteristics, and the specific applications where they excel.
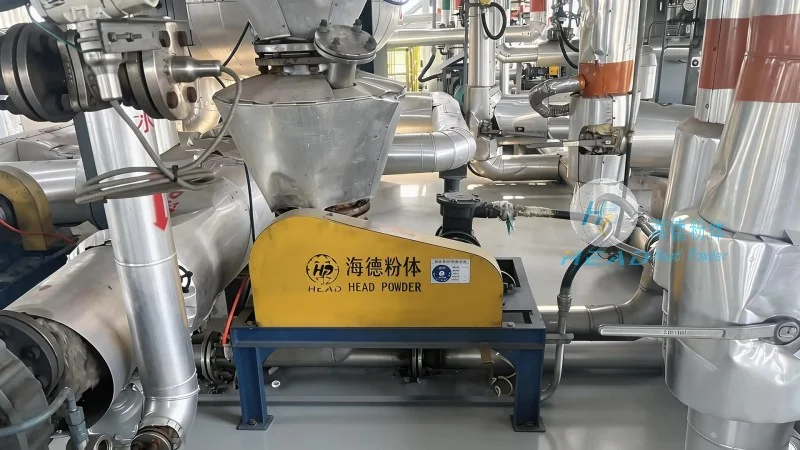
There are primarily two main categories of dust pneumatic conveying systems: pressure and vacuum systems. Each type operates on different principles and is suitable for distinct operational conditions.
Pressure systems, also known as positive pressure systems, utilize compressed air to push material through a pipeline. This method is ideal for applications requiring high material flow rates and the ability to transport materials over longer distances. The system operates by introducing high-pressure air into a hopper, which then forces the material into the pipeline. Pressure systems are commonly used in industries such as food processing, pharmaceuticals, and chemical manufacturing where product purity and contamination control are critical.
Vacuum systems, or negative pressure systems, use suction to draw material from a source into a collection point. This approach is particularly effective for handling materials that are difficult to move by pressure alone, such as those with high moisture content or those that tend to clog pipelines. Vacuum systems are often employed in applications like dust collection, where the goal is to capture and transport airborne particles to a designated storage or treatment facility. The system works by creating a low-pressure environment at the inlet, which pulls material from the source and transports it through the pipeline to a receiver.
Several critical characteristics define the performance and suitability of dust pneumatic conveying systems. These include material handling capacity, system pressure, pipeline design, and the ability to handle varying particle sizes and moisture content.
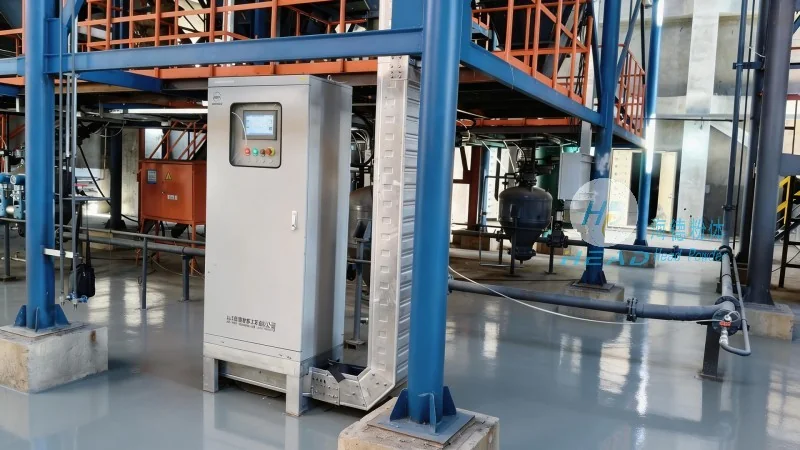
Material handling capacity refers to the volume of material that can be transported per unit time. This is influenced by factors such as the system pressure, pipeline diameter, and the type of material being conveyed. Higher pressure systems generally offer greater capacity, making them suitable for high-volume operations. For example, in a food processing plant, a pressure system might be used to transport large quantities of flour or sugar from storage silos to processing lines.
System pressure is another important characteristic. Pressure systems typically operate at pressures ranging from 2 to 10 bar, while vacuum systems may operate at pressures below atmospheric, often around -0.5 to -1 bar. The choice of pressure level depends on the material's properties and the distance to be covered. For instance, transporting fine powders over a distance of 100 meters might require a pressure system operating at 6 bar, whereas a shorter distance of 50 meters could be managed with a lower pressure of 3 bar.
Pipeline design is also a crucial aspect. The diameter and length of the pipeline, along with the number of bends and fittings, affect the system's efficiency and pressure drop. Proper design minimizes energy consumption and prevents material buildup or clogging. HeadPowder engineers carefully design pipelines to ensure smooth material flow, using appropriate diameters and minimizing the number of bends to maintain consistent pressure and prevent particle segregation.
The ability to handle varying particle sizes and moisture content is vital for many industrial applications. Some systems are designed to handle materials with a wide range of particle sizes, from fine powders to coarse granules. Others are specifically engineered to manage materials with high moisture content, which can cause clogging or degrade the system's performance. HeadPowder's systems incorporate features such as air classifiers and moisture control mechanisms to ensure reliable operation under diverse conditions.
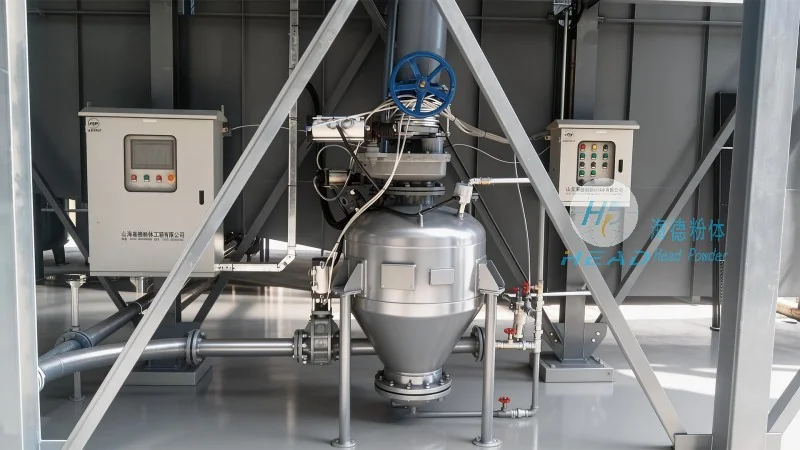
Dust pneumatic conveying systems find applications across a wide array of industries due to their versatility and efficiency. The specific type of system chosen depends on the material properties, operational requirements, and the environment in which it will be used.
In the food and beverage industry, these systems are widely used for transporting ingredients like flour, sugar, and spices. The pressure systems are preferred here because they can maintain product purity and prevent contamination. For example, in a bakery, a pressure system might be used to convey flour from storage bins to mixing machines, ensuring a consistent and clean process.
The pharmaceutical industry also relies heavily on dust pneumatic conveying for transporting active pharmaceutical ingredients (APIs) and other fine powders. The systems must meet stringent regulatory requirements for cleanliness and contamination control. Vacuum systems are often used in this sector to collect dust and particles from production lines, ensuring a safe and hygienic environment.
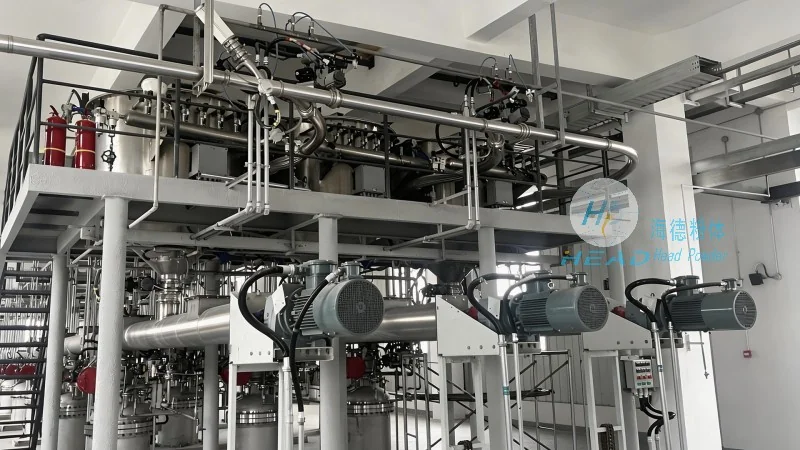
In the chemical and petrochemical industries, these systems are used to handle a variety of powders and granules, including chemicals, catalysts, and fertilizers. The pressure systems are suitable for transporting materials over longer distances and at high flow rates, while vacuum systems are used for dust collection and material recovery. For instance, in a fertilizer plant, a pressure system might be used to transport urea from storage silos to packaging lines, while a vacuum system collects dust from the production process.
The mining and minerals industry utilizes dust pneumatic conveying for transporting raw materials and byproducts. The systems are designed to handle abrasive and heavy materials, often with higher pressure and robust pipeline components. This ensures reliable operation in harsh environments where other conveying methods might fail.
In the construction and cement industry, dust pneumatic conveying is used for transporting cement, fly ash, and other powders. The systems are typically pressure-based and are designed to handle large volumes of material over medium distances. This method is more efficient than traditional methods like bucket elevators or belt conveyors, as it reduces labor costs and improves material handling speed.
Dust pneumatic conveying systems are a versatile and efficient solution for transporting fine powders and granular materials in various industrial applications. The choice between pressure and vacuum systems, along with the specific design features, depends on the material properties, operational requirements, and the environment. HeadPowder, with its expertise and facilities in Shandong, China, provides tailored solutions that meet the diverse needs of its clients, ensuring reliable and efficient material handling across different industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top