Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems. This article focuses on the design of a sulfur negative pressure pneumatic conveying system, highlighting key components, operational principles, and practical applications.
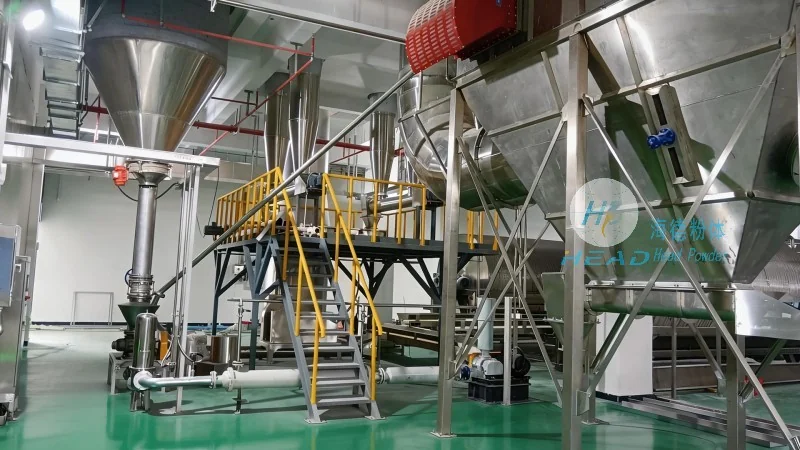
The sulfur negative pressure pneumatic conveying system is engineered to efficiently transport sulfur from storage silos or processing units to downstream equipment such as reactors or packaging facilities. This system operates under negative pressure, meaning the conveying pipeline maintains a lower pressure than the ambient environment, which helps in controlling dust emissions and ensuring safe material handling. The design incorporates robust materials and components suitable for handling sulfur's physical properties, including its granular or powdered form, and the system is built to meet industrial standards for reliability and performance.
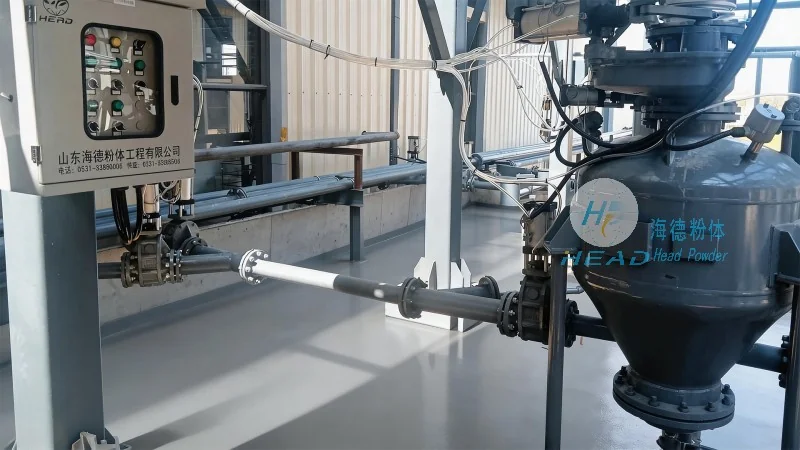
The system's core components include a negative pressure blower, a conveying pipeline network, a dust collection system, and a material feed hopper. The blower is selected based on the required air volume and pressure to ensure sufficient suction power to transport sulfur particles through the pipeline. The pipeline is typically made of corrosion-resistant materials like stainless steel or special coatings to withstand sulfur's chemical properties. The dust collection system, often equipped with cyclone separators or bag filters, is integrated to capture any fine particles and maintain air quality. The feed hopper is designed with a metering valve to control the flow rate of sulfur, preventing overloading and ensuring consistent conveying rates.
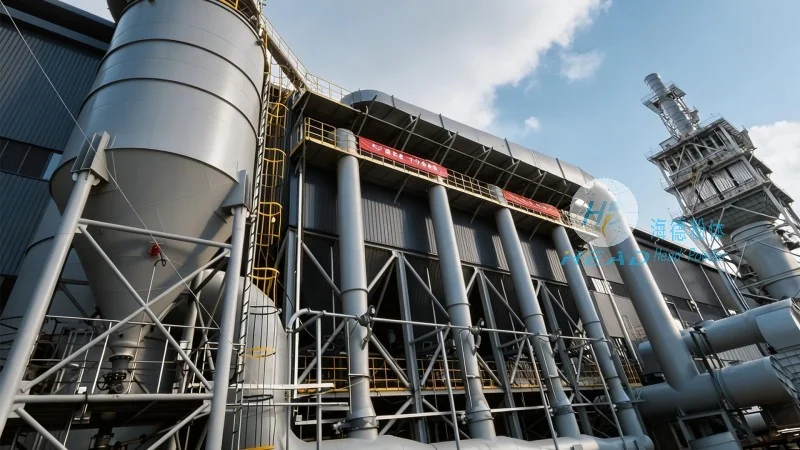
The negative pressure system works by drawing air and sulfur particles into the pipeline using the blower's suction. As the material moves through the pipeline, it is suspended in the air stream and transported to the destination. The design emphasizes energy efficiency by optimizing the blower's performance and minimizing pressure losses in the pipeline. This results in lower operational costs and reduced energy consumption compared to positive pressure systems. Additionally, the negative pressure operation helps in containing dust, reducing environmental impact and ensuring compliance with industrial safety regulations.
This sulfur negative pressure pneumatic conveying system is widely used in the chemical industry, particularly in sulfur processing plants. It offers several advantages over traditional methods such as belt conveyors or manual handling, including improved safety by reducing human exposure to sulfur dust, enhanced process control through precise material flow regulation, and increased efficiency by minimizing material handling time and losses. The system's modular design allows for easy integration into existing production lines and can be customized to meet specific plant requirements, such as varying sulfur feed rates or pipeline lengths.
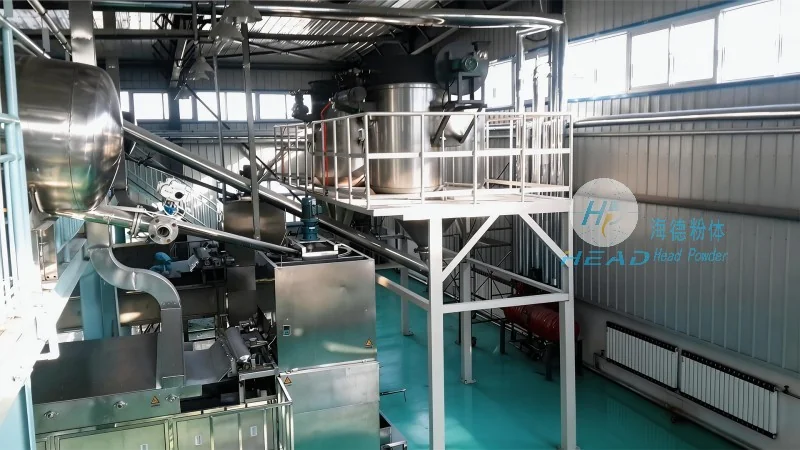
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions for sulfur negative pressure pneumatic conveying systems, combining advanced engineering, high-quality materials, and reliable performance. The design of this system ensures efficient, safe, and cost-effective transportation of sulfur, supporting the operational needs of chemical processing facilities. With a strong commitment to quality and customer satisfaction, HeadPowder continues to innovate in pneumatic conveying technology, delivering solutions that meet the evolving demands of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top