Desulfurization sodium bicarbonate is a critical component in modern industrial processes, particularly within the power generation and environmental protection sectors. The efficient and reliable transport of this material is essential for maintaining operational efficiency and ensuring compliance with environmental standards. Pneumatic conveying technology offers a sophisticated solution for handling desulfurization sodium bicarbonate, with both negative pressure and positive pressure systems providing distinct advantages and applications. This article provides a comprehensive overview of these pneumatic conveying methods, exploring their principles, operational characteristics, and practical applications in industrial settings.
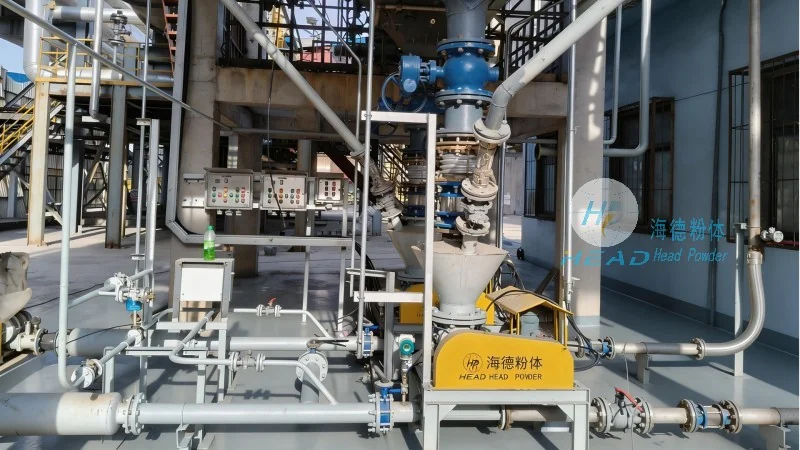
Pneumatic conveying is a method of transporting bulk materials through a pipeline using air or gas as the conveying medium. In the context of desulfurization sodium bicarbonate, this technology is employed to move the material from storage or processing units to reactors, silos, or other destinations. The two primary types of pneumatic conveying systems are negative pressure (or vacuum) systems and positive pressure systems, each with unique design considerations and operational benefits.
Negative pressure systems operate by creating a vacuum within the conveying line, which draws the material from the source into the system. This approach is particularly effective for applications requiring the transport of material over short to medium distances, typically up to several hundred meters. The vacuum created by the system ensures that the material is drawn into the pipeline without the need for high-pressure air, reducing energy consumption and minimizing the risk of material degradation. The design of negative pressure systems often includes a venturi or eductor that generates the vacuum, with the material being entrained by the airflow. This method is well-suited for handling fine powders and granular materials, such as desulfurization sodium bicarbonate, which can be prone to dust generation and clogging if not managed properly.
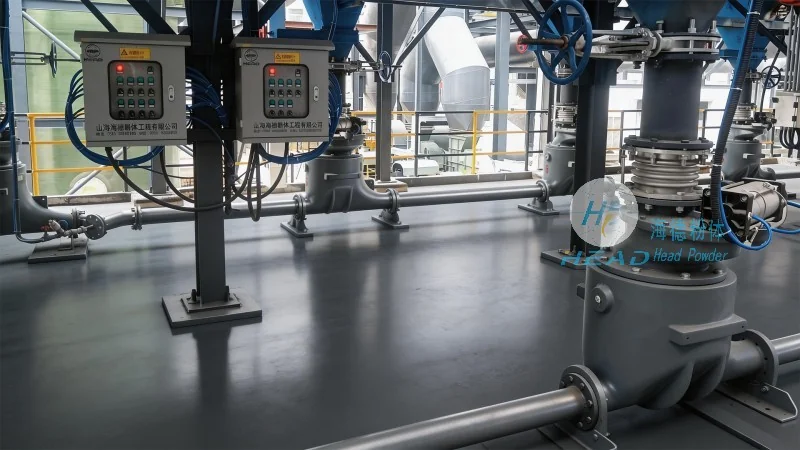
One of the primary advantages of negative pressure pneumatic conveying is its ability to handle materials that are sensitive to high pressures or temperatures. The low-pressure environment within the system helps preserve the integrity of the desulfurization sodium bicarbonate, preventing clumping or agglomeration that could affect its performance in downstream processes. Additionally, negative pressure systems are generally more cost-effective for shorter transport distances, as they require less robust equipment and lower air pressure. These systems are commonly used in applications where the material is sourced from a hopper or silo and needs to be delivered to a reactor or storage tank within a facility. The gentle handling of the material also reduces the risk of product degradation, making it an ideal choice for materials that are prone to moisture absorption or chemical changes.
Positive pressure systems, in contrast, operate by forcing air or gas under pressure through the conveying line, pushing the material from the source to the destination. This method is typically employed for longer transport distances, often exceeding several hundred meters, and is capable of handling a wider range of material types and flow rates. The high-pressure air or gas creates a positive pressure within the pipeline, ensuring that the material is propelled through the system with consistent flow rates. The design of positive pressure systems includes a blower or compressor that supplies the pressurized air, with the material being mixed with the air stream to form a slurry or suspension.
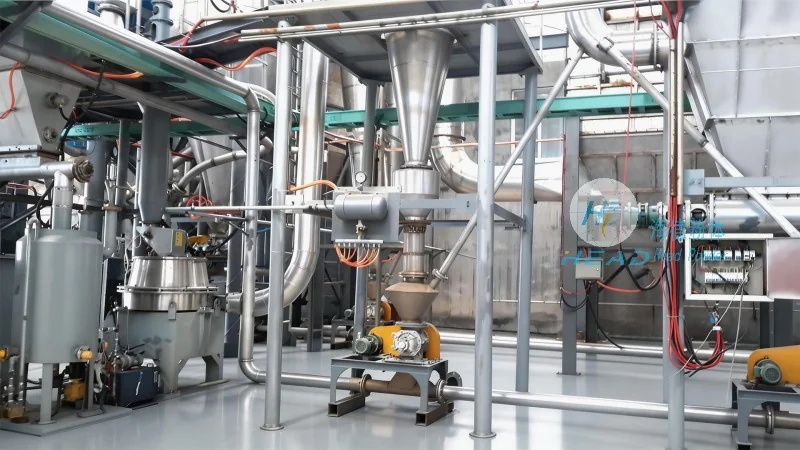
Positive pressure pneumatic conveying offers several advantages over negative pressure systems, particularly for longer transport distances and higher material throughput. The ability to maintain consistent pressure and flow rates allows for more reliable and efficient material transport, reducing downtime and operational costs. Additionally, positive pressure systems can handle a wider variety of materials, including bulkier or more abrasive particles, without the risk of clogging or blockage. This makes them suitable for applications where the desulfurization sodium bicarbonate needs to be transported over longer distances, such as from a central storage facility to multiple processing units within a plant. The high-pressure environment also helps prevent dust emissions and material loss, enhancing safety and environmental compliance.
When selecting a pneumatic conveying system for desulfurization sodium bicarbonate, it is essential to consider the specific requirements of the application, including distance, material characteristics, and operational constraints. The choice between negative and positive pressure systems depends on several factors, such as the required transport distance, the material's flow properties, and the available space for equipment installation. Negative pressure systems are generally more suitable for shorter distances and materials that are sensitive to high pressures, while positive pressure systems are preferred for longer distances and higher material throughput. The cost of equipment and maintenance also plays a significant role in the decision-making process, as positive pressure systems may require more robust components and higher energy consumption.
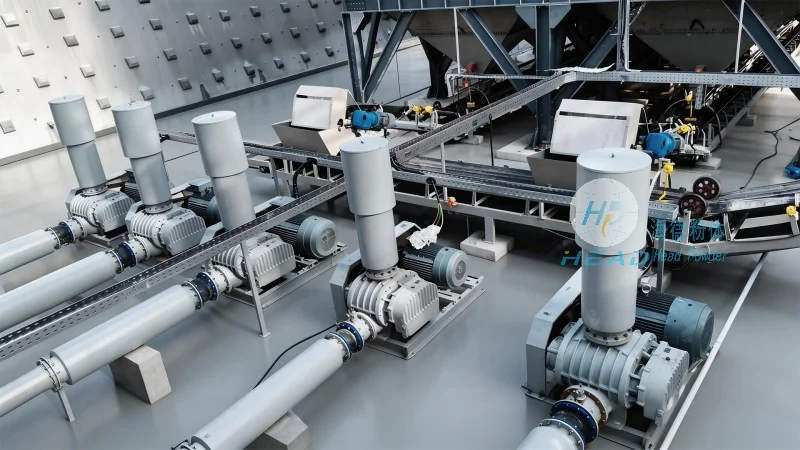
The application of pneumatic conveying technology for desulfurization sodium bicarbonate has been successfully implemented in various industrial settings. For example, in power plants, desulfurization sodium bicarbonate is transported from storage silos to the desulfurization reactors using negative pressure systems, ensuring efficient and reliable material delivery. In chemical processing facilities, positive pressure systems are used to transport the material from a central processing unit to multiple reactors, maintaining consistent flow rates and minimizing material loss. These applications demonstrate the effectiveness of pneumatic conveying in improving operational efficiency and reducing downtime, while also enhancing safety and environmental compliance.
In conclusion, pneumatic conveying technology provides a reliable and efficient solution for transporting desulfurization sodium bicarbonate in industrial applications. The choice between negative and positive pressure systems depends on the specific requirements of the process, including distance, material characteristics, and operational constraints. By understanding the principles and advantages of each system, industrial facilities can select the most appropriate pneumatic conveying method to optimize their operations. The implementation of these systems, as demonstrated by successful case studies, has led to improved efficiency, reduced costs, and enhanced safety in the handling of desulfurization sodium bicarbonate. As industrial processes continue to evolve, the continued development and application of advanced pneumatic conveying technologies will remain critical for maintaining operational excellence and environmental compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top