HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the efficient transport of carbonaceous particles over extended distances. This system represents a sophisticated solution that integrates cutting - edge technology with robust engineering principles to ensure reliable, low - maintenance operation in industrial settings.
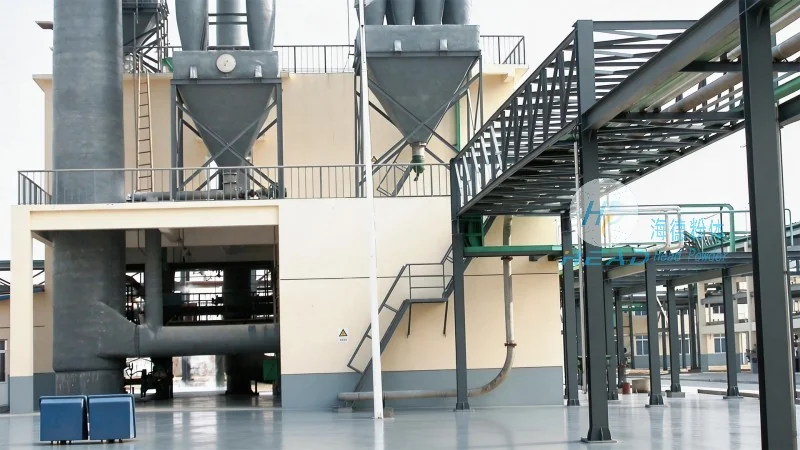
The system comprises several key components, each meticulously engineered to optimize performance and durability. The primary elements include a high - capacity air compressor, a series of flexible or rigid pipelines, and specialized hopper and receiver units. The air compressor generates the necessary pressure to move the carbonaceous particles through the pipeline, while the pipeline network is designed with considerations for material flow, pressure drop, and system efficiency. The hopper, typically equipped with a feeder mechanism, ensures a consistent feed of particles into the system, preventing blockages and maintaining steady flow rates. The receiver unit, often with a dust collection system, safely captures the particles at the destination, minimizing environmental impact and ensuring product integrity.
One of the standout features of this pneumatic conveying system is its exceptional efficiency in transporting carbonaceous particles over long distances. By utilizing compressed air as the conveying medium, the system eliminates the need for mechanical components like conveyors or elevators, which can be prone to wear and tear and require frequent maintenance. This pneumatic approach not only reduces operational costs but also enhances the overall reliability of the system. Performance metrics such as conveying capacity, pressure drop per unit length, and energy consumption are carefully optimized during the design phase. The system is capable of handling a wide range of particle sizes and densities, from fine powders to larger granules, making it versatile for various industrial applications. Additionally, the system's ability to maintain consistent flow rates and minimize material degradation during transport is a significant advantage, ensuring that the carbonaceous particles reach their destination in optimal condition.
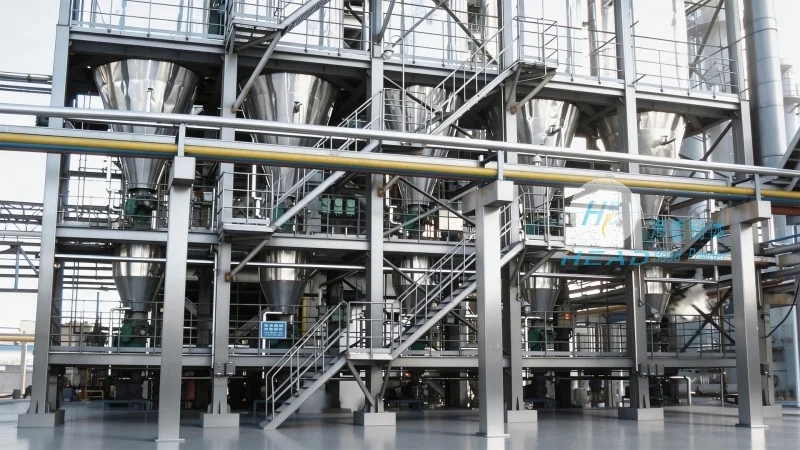
HeadPowder recognizes that industrial requirements vary widely, and thus, the long - distance pneumatic conveying system is highly customizable to meet specific client needs. The system can be adapted for different particle types, such as graphite, carbon black, or other carbon - based materials, by adjusting the pipeline diameter, air pressure, and feeder design. For applications requiring higher conveying rates or longer distances, the system can be scaled up with additional compressors or pipeline sections. The flexibility also extends to the system's layout, allowing for both horizontal and vertical conveying configurations, as well as complex network designs that integrate multiple source and destination points. This adaptability makes the system suitable for a broad spectrum of industries, including chemical manufacturing, battery production, and material processing, where the reliable and efficient transport of carbonaceous materials is critical.
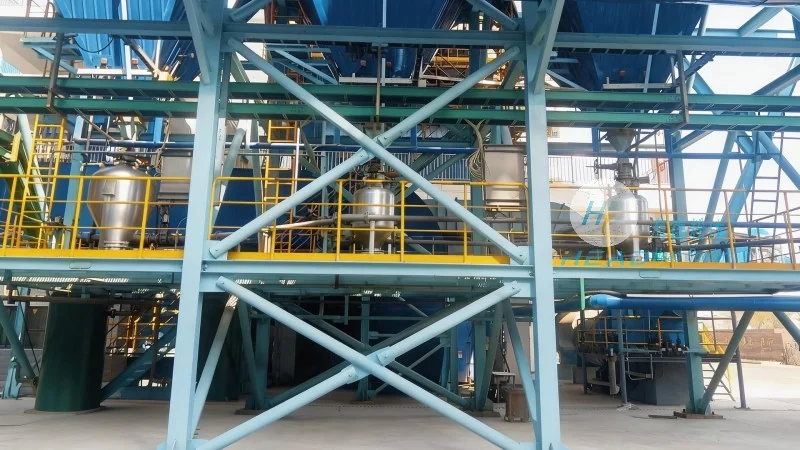
Reliability is a top priority in the design and operation of the long - distance pneumatic conveying system. The components are constructed from high - quality materials, such as stainless steel and corrosion - resistant alloys, to withstand the abrasive nature of carbonaceous particles and the effects of compressed air. Regular maintenance is essential to ensure the system's longevity and performance. HeadPowder provides comprehensive maintenance services, including routine inspections, component replacement, and system tuning. The system is equipped with monitoring and control systems that allow for real - time tracking of pressure, flow, and other critical parameters. This enables operators to detect potential issues early and take corrective action, minimizing downtime and maximizing system uptime. The low maintenance requirements, combined with the system's robust design, contribute to its long - term cost - effectiveness and reliability in industrial operations.
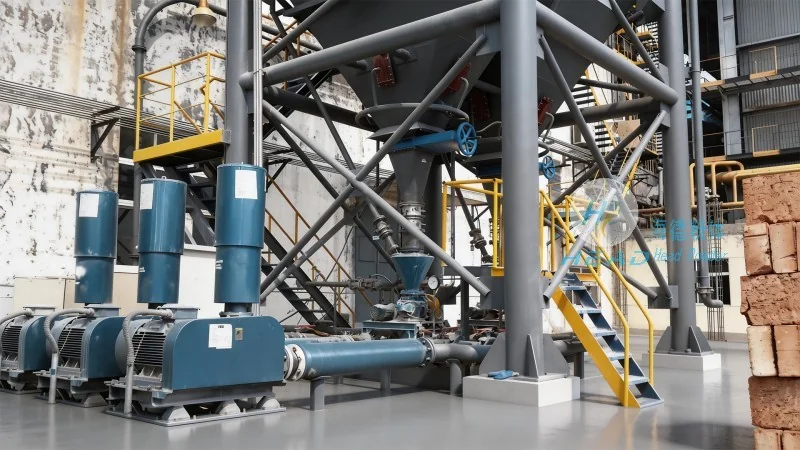
HeadPowder places a strong emphasis on environmental and safety compliance in the design and operation of the pneumatic conveying system. The system incorporates dust collection and filtration systems to minimize the release of airborne particles into the environment, ensuring compliance with local and international environmental regulations. The receiver units are designed with safety features, such as pressure relief valves and explosion - proof components, to prevent accidents and protect personnel. The system's operation is also designed to minimize energy consumption, aligning with sustainable industrial practices. By adhering to strict safety and environmental standards, HeadPowder ensures that the long - distance pneumatic conveying system not only meets operational requirements but also contributes to a safer and more sustainable industrial environment.
The long - distance pneumatic conveying system for carbonaceous particles, developed by Shandong HeadPowder Engineering Co., Ltd., represents a state - of - the - art solution for efficient material transport in industrial applications. With its robust design, high efficiency, and adaptability, the system addresses the challenges of transporting carbonaceous materials over extended distances while maintaining product quality and operational reliability. HeadPowder, with its expertise in engineering and commitment to quality, provides comprehensive solutions that cater to the diverse needs of its clients. Based in Shandong, China, HeadPowder continues to innovate and advance the technology of pneumatic conveying systems, contributing to the growth and efficiency of industries that rely on the reliable transport of carbonaceous materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top